
Europe's Cobot Boom: SME Automation and a Fragmented Cable Market
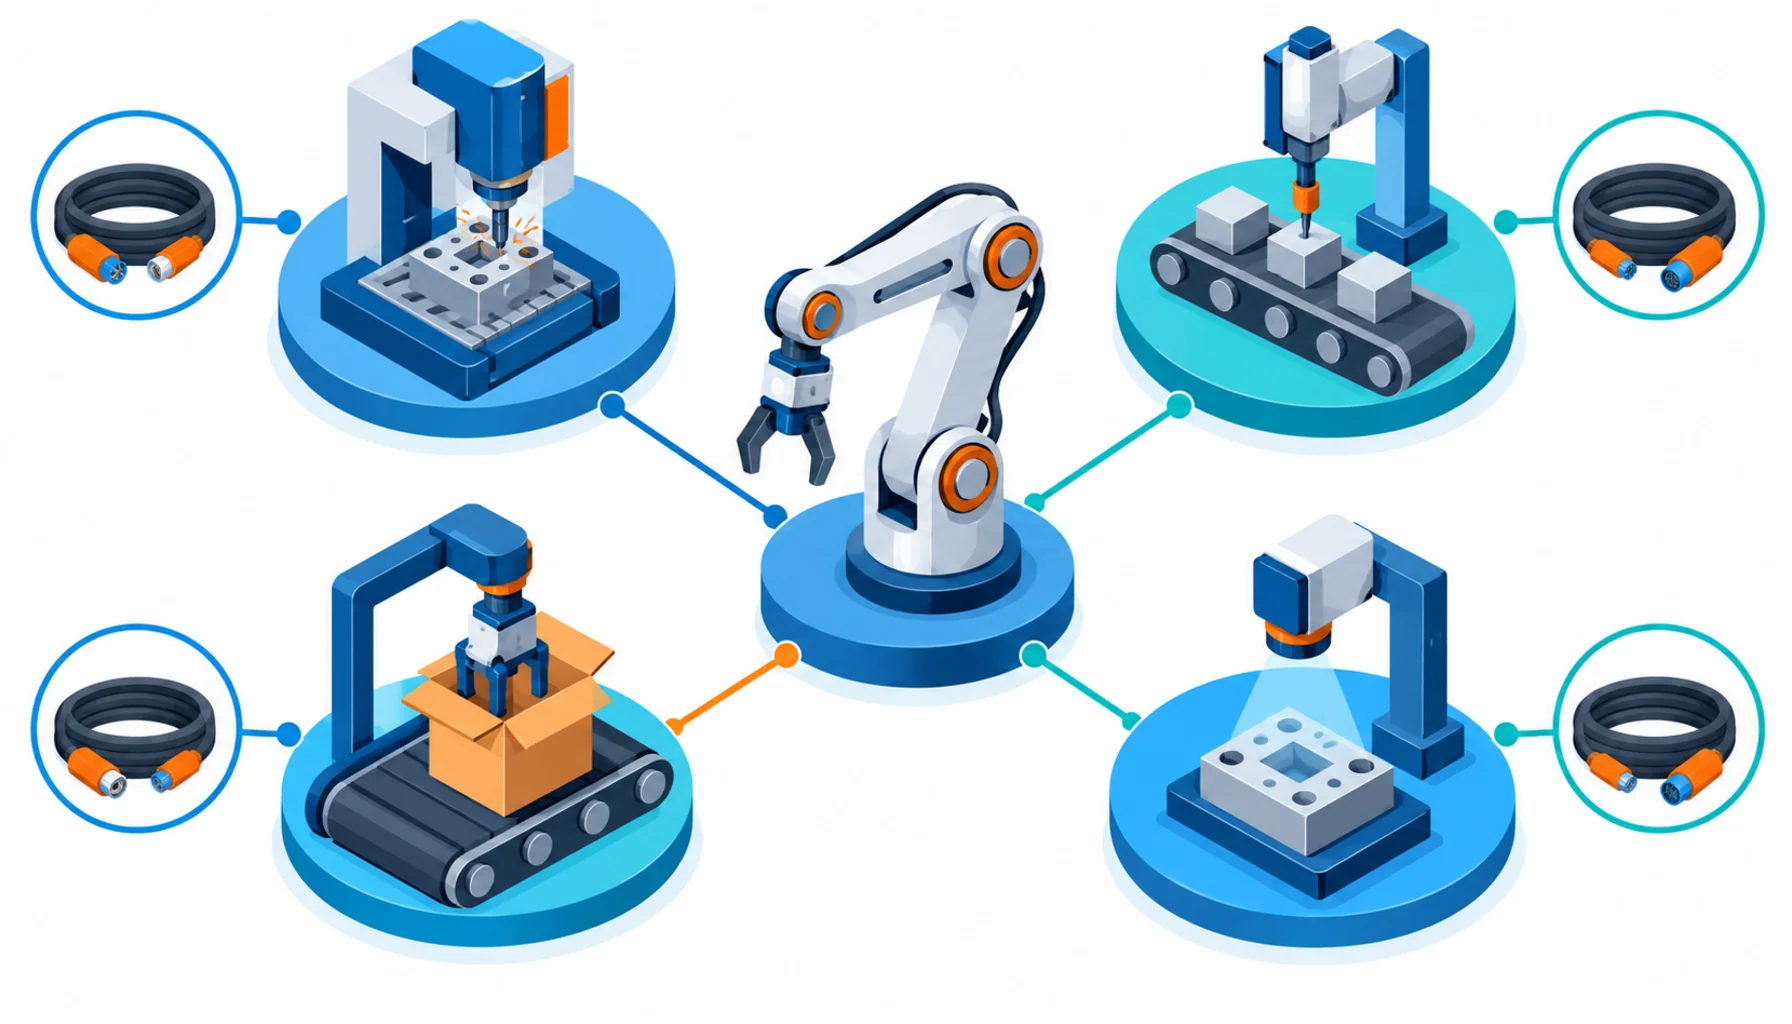
Quick Answer: Europe’s small and mid-sized manufacturers are automating with collaborative robots, and thousands of small cells across a fragmented market are quietly building steady motion cable demand.
The robot story Europe tells about itself is not the megafactory story Asia tells. It is a workshop story: a forty-person machining firm near Stuttgart, a packaging contractor in the Dutch countryside, a furniture shop in northern Italy, each putting one or two collaborative robots where a worker used to stand. Individually, none of these cells moves a market statistic. Collectively, they are reshaping European automation, and because a cobot cell is still a moving machine with flexing cable, they are reshaping cable demand in a distinctly European way: small orders, wide variety, and standards inherited from a dozen different machine-building traditions.
Introduction
The scale comes from breadth rather than depth. IFR’s World Robotics 2026 counts Germany alone for roughly 41 per cent of European Union installations, with the rest of the bloc, plus the United Kingdom, Switzerland and the Nordic countries, adding thousands of installations across hundreds of industries. Collaborative robots claim a growing share of those units, because they answer the question European SMEs actually ask: how do we automate a cell that sits metres from a worker, without fencing, guarding projects or a systems engineering degree. The safety framework for those cells, ISO/TS 15066 among others, is treated in its own guide; this article stays on the demand and cable side.
For cable suppliers, the European cobot market is the opposite shape to a gigafactory. No single order is large. There are thousands of small ones, spread across languages, machine builders and expectations, and the suppliers who serve them well are organised for variety rather than volume. That structure has consequences worth understanding before quoting.
Why the Cobot Suits the European SME
European small manufacturers face a specific automation problem. Their batches are small, their products change often, and their floors are full already, so a traditional robot cell with fencing, safety scanners and a concrete foundation is a project they postpone indefinitely. A collaborative robot answers differently: it bolts to a bench, installs in days, and its safety case is built into the machine itself. The economics follow from labour dynamics rather than production volume, and with European wages high and vacancies in skilled trades persistent, the payback calculation keeps improving.
The supply chain serving these buyers is itself fragmented. Cobots arrive from a handful of global brands, but the cells around them are built by regional integrators and small machine builders, each with their own cable philosophy. Some build to German norms, some to Scandinavian modular standards, some to whatever the local market tolerates. A cable supplier facing this market meets not one specification but a spectrum, and the ability to match construction to whatever standard the integrator carries becomes the core competence.
What a Cobot Cell Actually Asks of Cable
A cobot is a smaller machine than an industrial arm, but its cable duty is not proportionally smaller. The joints rotate through wide arcs, the dress pack is compact, and the space between the arm and the controller is short, which forces tighter bend radii than a large cell would accept. Payloads are light, so cable mass matters: a heavy cable drags on a light arm and disturbs the force sensing the cobot uses for safety. And the cell’s whole point is proximity to people, which makes the quiet failure of a cable, an intermittent encoder glitch or a sporadic stop, far more visible and far less tolerable than in a fenced cell.
Three cable properties therefore decide most European cobot orders. The first is compactness: smaller outer diameters and stiffer-or-softer jacket choices matched to the arm’s cable management. The second is cycle life at tight radius, evidenced rather than claimed, since integrators have all seen a cheap cable fail inside warranty. The third is signal quality: cobots carry force, torque and safety-rated signals through the same compact bundle as power, so the shield and grounding discipline described in the guide to control versus instrumentation cable applies inside a dress pack barely wider than a thumb.
| Application | Typical SME setting | Cable duty profile | Deciding property |
|---|---|---|---|
| Machine tending | Machining shops, injection moulders, job shops | Continuous cycles, moderate radii, mixed power and signal cores | Cycle life at the real radius |
| Assembly and gluing | Electronics, appliances, furniture, textiles | Wide joint arcs, compact dress pack, force-sensing signals | Compactness and shield quality |
| Packaging and palletising | Contract packers, food processors, wholesalers | Longer reaches, higher payloads, washdown in food settings | Jacket chemistry per environment |
| Quality and inspection | Test benches, measurement cells, laboratory automation | Short strokes, high counts, sensitive low-level signals | Signal integrity in motion |
Serving a Fragmented Market
The table shows the other feature of the cobot market: environments vary as widely as the applications. A food packaging cobot needs washdown-rated jackets; a machining cobot needs coolant and chip resistance; a laboratory cobot needs nothing exotic mechanically but everything precise electrically. Volume suppliers to this market keep a portfolio, not a flagship. The mechanical reasoning behind matching jacket and construction to environment is the same discipline set out in the analysis of common cable failure causes.
When the Cobot Story Is Not the Answer
The commercial structure of the European cobot market selects for particular supplier behaviour. Small orders punish logistics overhead, so suppliers who consolidate shipments, hold semi-finished stock of common constructions, or serve integrators through regional distributors keep their economics viable. Variety punishes rigid production, so suppliers with flexible stranding and extrusion capability, able to run short lengths of unusual constructions, capture the long tail. And the safety-adjacent nature of cobot work punishes vagueness, because integrators whose cells sit next to workers need documented evidence, not catalogue adjectives, before a cable goes into a dress pack.
Two structural facts help outside suppliers. First, the integrator layer is pragmatic: it judges cable by performance in the cell, not by nationality, and a supplier who supports a regional integrator well becomes its default for the next fifty cells. Second, the market’s fragmentation means no single qualification gate controls access, unlike the automotive or semiconductor chains; the entry ticket is honest evidence and reliable delivery, supported by the groundwork in the comparison of OEM and ODM supply models and, where machines ship onward, the certification overview in the cable certification checklist. Cabinet and bench wiring for these cells follows the build principles in the guide to custom control cabinets.
| Decision | Why it matters here specifically | Practical handling |
|---|---|---|
| Portfolio breadth | Applications and environments vary cell by cell | Maintain constructions for washdown, coolant, cleanroom-adjacent and dry duty |
| Small-order economics | Thousands of small cells replace a few large orders | Consolidate shipments; hold semi-finished stock; support distributors |
| Evidence for safety-adjacent work | Cells operate beside workers; failures are visible and scrutinised | Document flex life, shields and ratings to a standard the integrator can file |
| Integrator partnership | The integrator chooses cable for dozens of end users | Support the integrator layer directly; become its default |
| Dimensional fit | Cobot cable management is compact and unforgiving | Confirm outer diameter, bend stiffness and connector fit against the arm |
RFQ Checklist: Cable for a European Cobot Project
Three cautions. First, collaborative does not mean cable-light: a cobot cycles just as often as an industrial arm, sometimes more, and treating its dress pack as an accessory has cost more than one European integrator a warranty season. Second, the fragmented market resists standardisation quietly but not formally: where a cell’s machinery ships to other markets, the parent standards and their paperwork return, so the certification checklist still applies. Third, the SME price sensitivity is real; the winning offer is not the cheapest cable but the one whose failure cost is obviously higher than its premium, a case integrators make to their customers with the supplier’s evidence.
Conclusion
Send these so the quote fits the cell and the market:
- Cobot model and payload class, with the cable management style used on the arm
- Duty: strokes, joint arcs, cycles per shift, and whether the cell runs unattended nights
- Outer diameter, bend stiffness and connector constraints of the dress pack
- Signal set carried: power, brake, force and safety-rated cores, and their shield needs
- Environment: washdown, coolant, dust or cleanroom-adjacent duty
- The integrator’s build standard or the machine parent’s specification, if any
- Order pattern: one cell now, a fleet later, or a call-off agreement across projects
- Evidence requirements the integrator must file with its own customer


