
Data Center Cabling Checklist for EPC Contractors
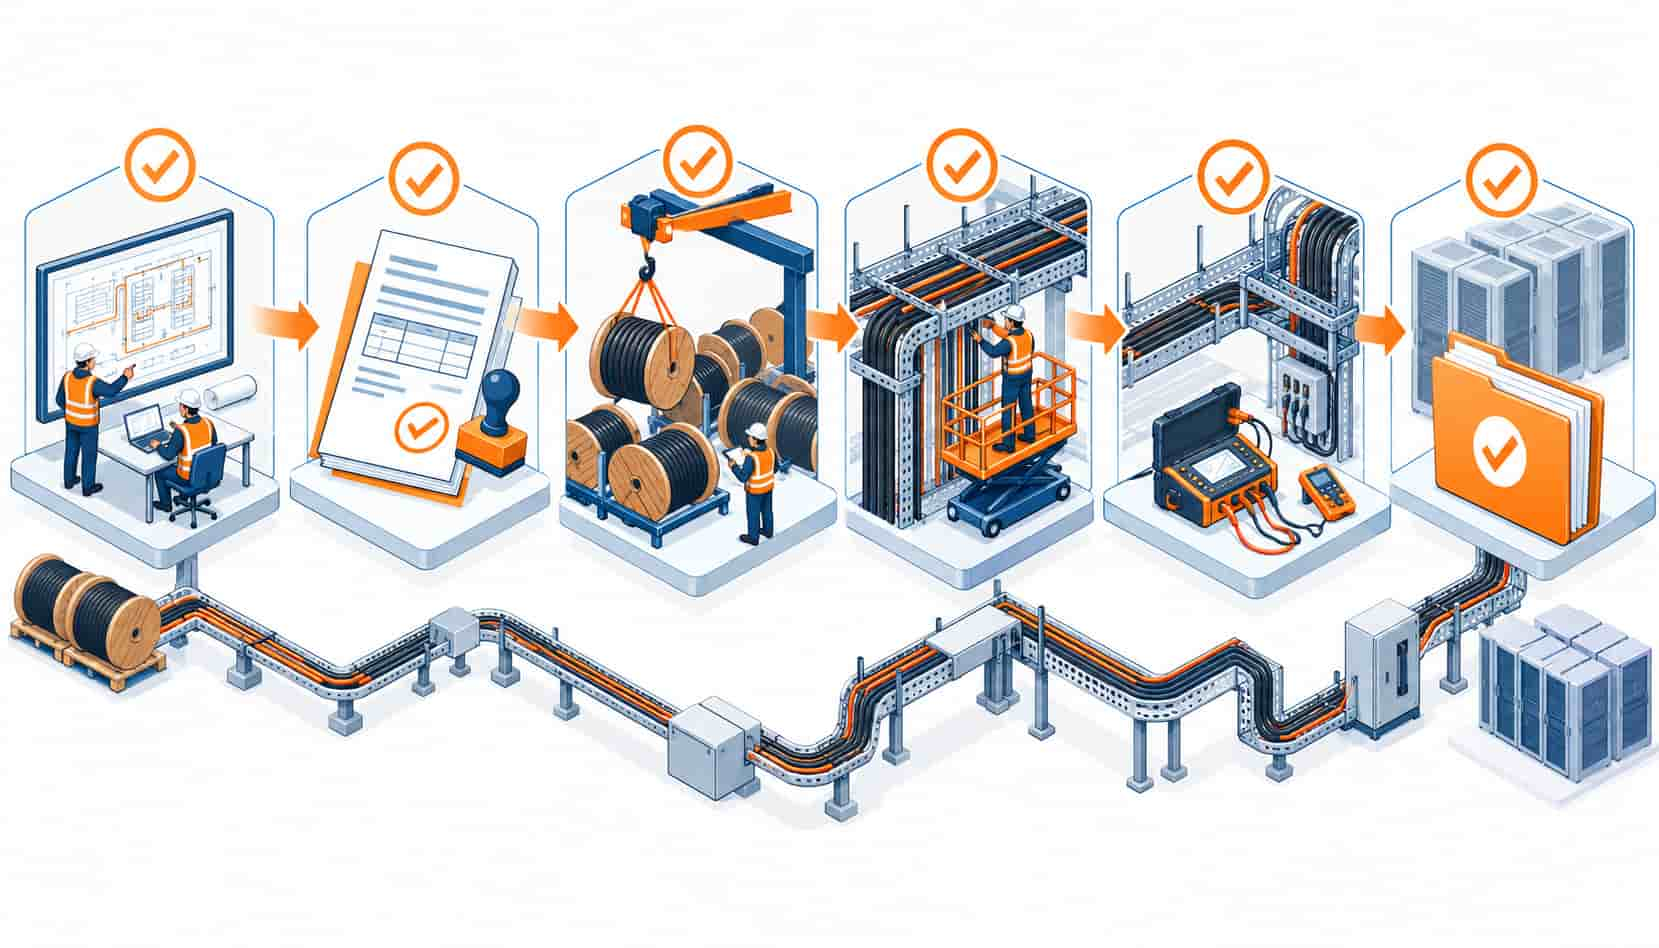
Quick Answer: A cabling project succeeds on six checkpoints: locked design inputs, delay-proof procurement, factory inspection, supervised installation, test records, and a handover file closed with the last feeder. Cable is the most underrated schedule risk in a data center package. It touches every discipline — civil routes, containment, switchgear terminations, commissioning sequence — yet it's usually the last major scope to be specified and the first to get blamed when dates slip. Contractors who deliver cleanly treat cabling as a phase-gated process. Each phase has a checklist, and the checklist closes before the next phase opens.
Introduction
This article is that checklist, written the way EPC projects actually run. It follows the phases — design, procurement, factory, installation, testing and handover — and each section lists what must be verifiably true before the phase closes, plus the deliverable that proves it. Use it as a review aid at gate meetings; the RFQ checklist at the end turns the same logic into what you send suppliers. The broader sourcing context these phases sit inside is covered in our guide to sourcing power equipment for EPC projects, and the facility-side scope in the data center power collection.
| Phase | Checklist Items | Phase Deliverable |
|---|---|---|
| Design | Load basis, derating, separation scheme, fire map, routed lengths | Frozen cable schedule and routing drawings |
| Procurement | Spec-to-schedule match, copper linkage, lead times, phasing plan | Awarded order with delivery calendar |
| Factory | Batch certs, sample tests, drum lengths, labeling, FAT findings | Inspection release notes per batch |
| Installation | Route conformity, pulling tension, separation kept, labeling live | Installation records per route |
| Testing | IR, continuity, torque, phasing, thermography baseline | Test reports keyed to circuit IDs |
| Handover | As-built match, spares list, documentation set complete | Signed as-built and O&M documentation file |
Design Phase: Inputs That Lock the Scope
Close the design phase with a frozen cable schedule, because everything downstream inherits from it: containment quantities, drum lengths, delivery phasing. Verify the load basis per circuit (measured or calculated load, battery recharge contribution, stated growth), the derating arithmetic per tray section, the separation scheme between cable families, and the fire-performance map per area. Routed lengths deserve real measurement. A walking survey with a measuring wheel beats a floor-plan estimate every time it’s tried, because routes never run as straight as drawings pretend.
The gate question for this phase is blunt: could a supplier quote from this document without calling you? If the schedule still carries “TBD” loads, estimated lengths or an unmapped fire class, the gate is not closed — and every quote that comes back will be a negotiation in disguise.
Procurement Phase: Documents That Prevent Delays
Cable procurement failures are rarely electrical; they’re calendar failures. Align the cable order with the master schedule — lead times against equipment delivery dates, deliveries phased to installation fronts, drum lengths matched to the measured routes — and lock the commercial mechanics: copper price linkage across the delivery calendar, verified copper content, test documents due with each batch rather than on request. The delay mechanics specific to cable, and the lead-time interplay with switchgear and transformers, are analyzed in our cable sourcing delays guide.
Decide in this phase what gets inspected at the factory, too. Cable FAT participation is not automatic in most contracts; the scope, timing and travel have to be written into the award, because the option to witness production is gone once production has happened.
Factory Phase: Inspect Before It Ships
Factory acceptance for cable is lighter than for switchgear but follows the same logic: verify at origin what would be costly to discover on site. Batch certificates for copper and materials, sample test results against the specified standards, drum length verification against the route schedule, drum labeling by route ID, sheath printing legibility — all of it belongs on the inspection sheet. The rationale for inspecting at the factory rather than the dock is the same one that governs equipment FATs, set out in our FAT versus SAT guide and the deeper case in why FAT testing matters.
The phase deliverable is an inspection release note per batch: what was checked, what was found, what the supplier corrected before shipment. That note is also the project’s first line of defense in any later material dispute. The batch was verified once, and the record exists.
Installation Phase: Supervision and Route Discipline
Installation quality is supervision quality. The items that matter: routes built as drawn (separation distances kept, barriers installed, bend radii respected), pulling tensions within manufacturer limits with the lubrication and rollers that implies, glands and terminations installed by trained hands with the correct kits, and labeling applied as the route is completed — not as a heroic re-walk at the end. Every route gets an installation record: as-installed path, lengths pulled, deviations approved in writing, crew and date.
The discipline pays a schedule dividend, too. Routes that conform install once. Routes that improvise come back during testing as continuity faults, interference complaints and re-pulls.
Testing and Handover: Records That Close the Project
Test records get generated as work proceeds, not commissioned at the end: insulation resistance and continuity per circuit as each route completes, torque verification at terminations, phasing checks before energization, and a thermography baseline scan under first load — the reference every future scan gets compared against. Reports are keyed to circuit IDs, so any record traces to its physical feeder in one step.
Handover closes with three artifacts: an as-built that matches the field (verified by sampling routes against drawings), a spares list matched to the installed constructions, and the complete documentation file — schedules, certificates, test reports, installation records, thermography baseline. Projects that produce these three artifacts hand over in a day. Projects that don’t, hand over eventually. For suppliers able to coordinate the full scope — cable, switchgear, transformers with one documentation standard — the single-supplier logic is compared in our one-stop sourcing guide.
| Check Item | Requirement | Why It Matters |
|---|---|---|
| Schedule frozen | No TBD loads, lengths measured on route | Quotes against guesses are negotiations |
| Standards named | Test classes and fire map per area stated | Named standards quote faster than adjectives |
| Delivery calendar attached | Phases matched to installation fronts | Cable on time is cable that installs |
| Commercial mechanics set | Copper linkage, verification rights, document dues | Metal speculation is not an engineering plan |
| FAT scope written | Inspection items, timing and attendance in the award | Unplanned inspections do not happen |
| Documentation duty explicit | Batch reports due with delivery, keyed to IDs | Records requested later arrive never |
When a Checklist Is Not the Answer
A checklist organizes decisions; it doesn’t make them. If the project’s cable scope crosses standards regimes, mixes MV and LV with unusual separation constraints, or lands on a compressed schedule with supplier lead-time risk, the honest next step is engineering support from the supplier side — a specification review before award, a joint route survey, a delivery plan built with the production planner rather than a sales desk. The failure pattern it prevents is a familiar one: a compliant quotation against an ambiguous spec, an award, then six weeks of discovering the two parties bought different projects.
Checklists also can’t rescue a scope that was never resourced. If nobody owns the cable documentation duty, no inspection trip is budgeted and no supervision hours exist, the checklist becomes a description of things that won’t happen. Assign the owner first, then use the list.
RFQ Checklist: Send This to Your Cable Supplier
The request that gets fast, quotable answers includes:
- Frozen cable schedule: circuit, voltage, load basis, routed length per run
- Derating table per tray section, shown with the resulting ampacities
- Fire-performance map: construction and standard class per area
- Applicable standards named: IEC/GB/BS as the project requires
- Accessory schedule: glands, lugs, kits matched to landing equipment
- Delivery calendar phased to installation fronts, drums labeled by route
- Copper price linkage across the delivery calendar
- Batch certificates and test reports due with each delivery, keyed to IDs
- FAT scope: inspection items, timing, attendance written into the award
- Supervision or specification review offered as a quoted line item
Ready to put the checklist to work? Request a cable quotation with your schedule attached, and you’ll get an engineering-reviewed answer rather than a price list.
Conclusion
EPC cabling is a chain of six gates — design, procurement, factory, installation, testing, handover — and each gate carries a short list of items that must be verifiably true before it closes. Contractors who work the gates deliver cable nobody remembers. Contractors who skip them deliver cable everybody talks about.
Kexingyu Cable Group (KXYE) works this checklist from the supplier side: engineering-reviewed quotations, phased deliveries matched to installation fronts, batch documentation keyed to circuit IDs and copper price linkage across the calendar — so the cable scope clears its gates on the first pass.


