
Cable Labeling and Documentation for Data Center Handover: What to Specify and What to Check
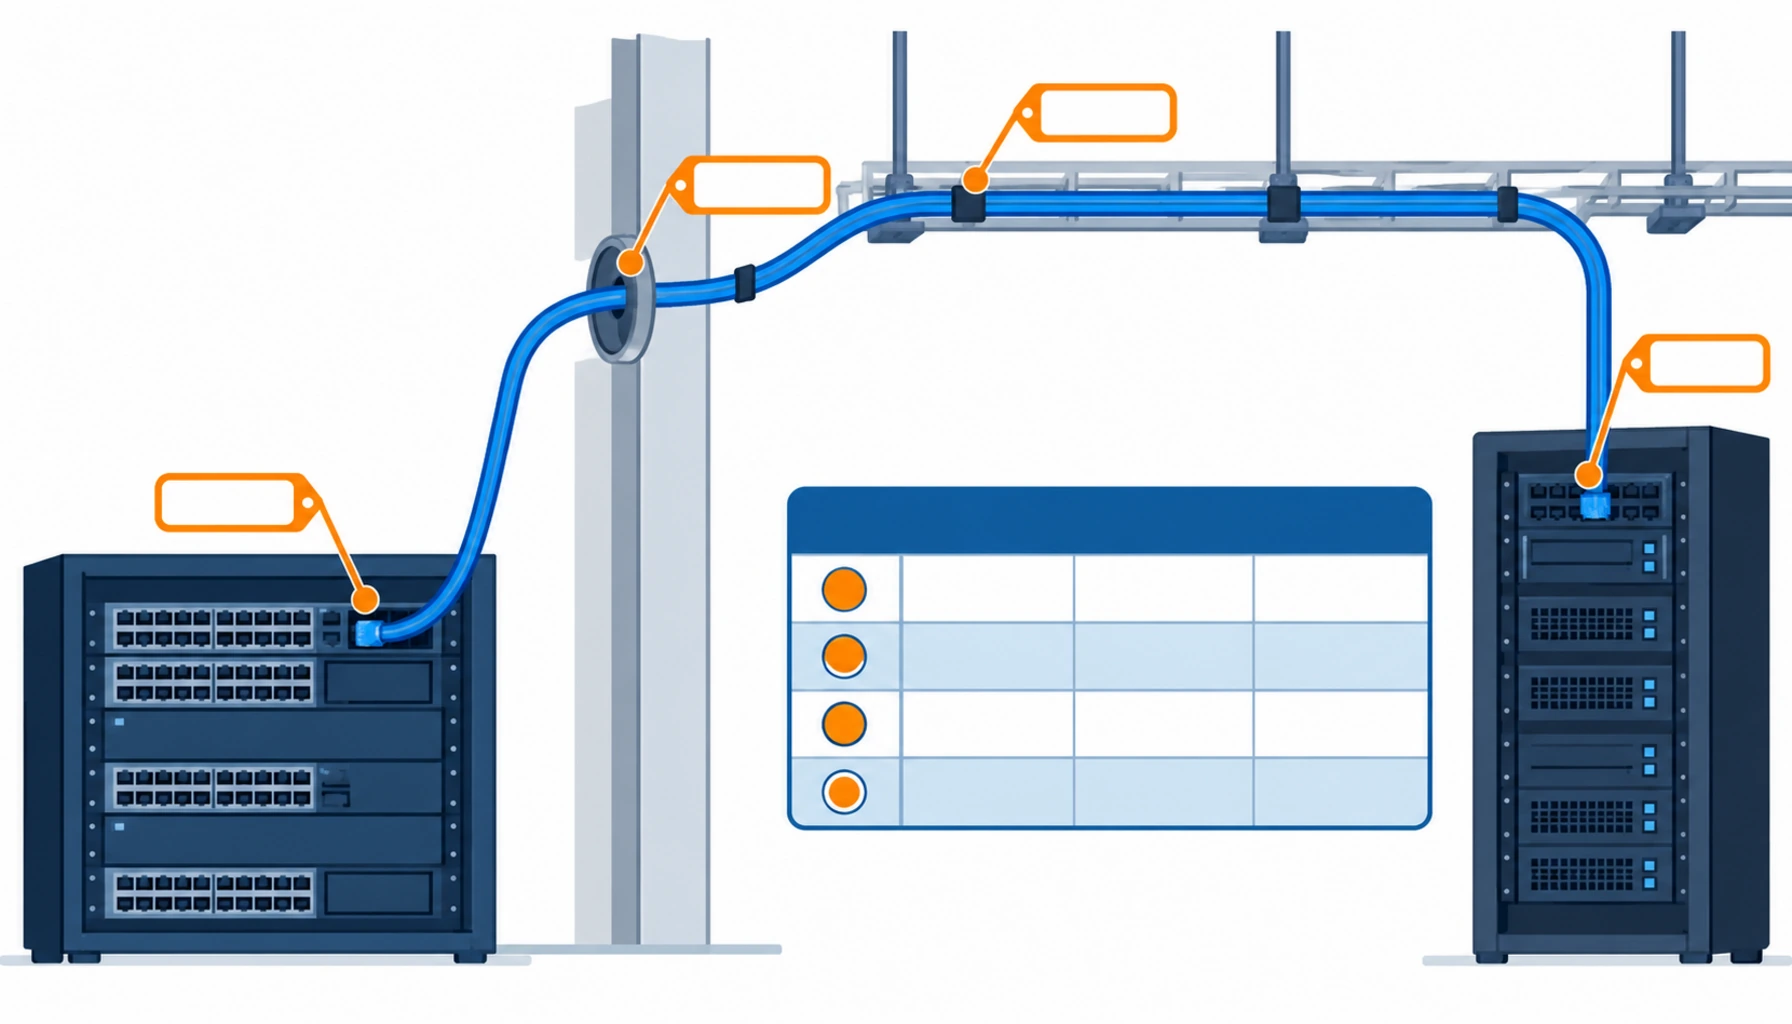
Quick Answer: Identification is the cheapest item in a cabling package and the one that decides how expensive every future change will be. Three specification lines carry most of the value: the label material and print method, because a label that falls off in a plenum has cost more than it saved; the position rule, so that every cable is identified at both ends and at each penetration and tray exit; and the document format, which must be editable rather than scanned. Ask for a naming convention agreed before installation starts, and the schedule becomes the asset register instead of a document nobody can use.
Nobody buys a data center because of its cable labels. They become visible in a different way: when a circuit has to be isolated for maintenance and the technician cannot read the identification, or when a schedule says one thing and the installation says another, and the only safe response is to trace the cable physically. That tracing costs hours of skilled labour, it occasionally costs an outage, and it happens repeatedly for the life of the building.
Introduction
Identification is unusual among cabling scope items because the cost is almost entirely labour rather than material. A good label costs a fraction of a good terminal, and the difference in price between basic and durable labels is small in absolute terms. What differs is the discipline: whether labels are printed rather than written, applied at defined positions, and recorded in a schedule that matches what was installed.
That makes labeling a specification purchase rather than a product purchase. The material matters, the print method matters, and the position rule matters most of all, because a labeled cable that is only labeled at one end is half identified. The documentation half is the same story: the deliverable is not the existence of a schedule, it is a schedule that somebody can update next year without retyping it.
Labels Fail for Predictable Reasons
Four failure mechanisms account for almost every unreadable cable in a data hall, and each has a specification answer.
The adhesive gives up. Labels applied to cable in a plenum or a hot electrical room are exposed to temperature cycling and to the airflow that carries dust. A general-purpose adhesive label eventually lifts at one edge and then disappears. Cable ties of the right material, or heat shrink sleeves, remove the adhesive from the equation entirely, which is why sleeves dominate in the applications where failure is expensive.
The print fades. Hand-written labels are the most common cause of unreadable identification, because the ink is not durable and the handwriting is not consistent. Direct thermal printing produces text that fades with heat and light over a period of years; thermal transfer printing with a suitable ribbon is the method that survives. The print method is worth stating explicitly rather than being left to whatever printer is on site.
The label is in the wrong place. A label applied a metre inside a tray is invisible, and a label applied only at the origin is useless at the destination. The position rule needs to be written: at both ends, at each penetration, at each tray exit and entry, and at intervals on long runs. The count of labels per cable is then a predictable number rather than a site decision.
The identification is not unique. Two cables carrying the same reference is worse than an unlabeled cable, because it produces confident wrong decisions rather than cautious ones. Uniqueness is a property of the naming convention, not of the label, and it is fixed before installation or not at all.
Factory Printing Versus Site Printing: Where the Money Is
Most power cable arrives with a legend printed along the sheath, typically carrying the model designation, the conductor size, the voltage rating, the standard it is made to, and often a metre marking. That legend is produced at the factory where printing costs almost nothing per metre, and it is not the same thing as a cable identification label, but the two are related.
Where a project can ask the supplier to include a project reference or a drum reference in the sheath legend alongside the standard data, the amount of site labeling work falls. The cable arrives on site already carrying information that ties it to a specific circuit group or drum, and the site work reduces to the end labels and the penetration labels, which are the labels that genuinely have to be applied after installation. On a large hall where the same cable type is used across hundreds of circuits, that reduction is measurable in labour hours rather than in material cost.
The question to put in the enquiry is straightforward: what information can be printed along the sheath, and can a project reference be included. Ask it before the order, because the legend is set at manufacture and cannot be changed afterwards. Our note on cables and wiring systems covers the constructions this applies to, and the control cable used for interlocking and monitoring follows the same practice.
The Decision Table: Identification Options Compared
The table compares how a project can buy identification. The last two columns describe what each option costs in labour and what happens when it fails.
| Option | What to Specify | Evidence You Receive | Cost and Labour Shape | Failure Mode If Chosen Wrong |
|---|---|---|---|---|
| Hand-written labels | The pen and label stock permitted, and the position rule | Labels in place; legibility varies with the writer | Lowest material cost, highest rework rate, no printing equipment needed | Unreadable identification within a few years, and physical tracing of every circuit |
| Site printed labels | Print method, ribbon, label material, and the content format for each position | Consistent printed labels, plus the printer's data file | Moderate equipment and setup cost, low marginal cost per label | Printer data not retained, so every future label has to be re-created by hand |
| Printed label plus factory sheath legend | What the supplier can print along the sheath, and whether a project or drum reference can be included | Sheath legend on delivery plus printed site labels | Lowest site labour; the legend is free once set at manufacture | A site labeling schedule far larger than it needed to be, because the ask was never made |
| Heat shrink sleeves and printed markers | Sleeve material, temperature range, print method, and the sizes required per cable | Sleeves applied and printed, with a sample approved before bulk order | Higher material cost, lower failure rate, best performance in plenum and hot locations | Adhesive labels used in locations where only a sleeve survives, and identification lost |
| Coded labels linked to an asset register | The code format, the resolution of the link to the schedule, and who maintains the register | Scannable identification plus the register export | Highest setup cost; pays back where the installation changes regularly | A register that is not maintained, so scans return records that no longer match reality |
The Document Set Is the Deliverable, Not the Spreadsheet
Every cabling project produces a cable schedule. What differs is whether that schedule survives contact with the next person who needs it.
The three characteristics that decide this are format, structure and reconciliation. Format means editable rather than scanned: a schedule delivered as a PDF is a read-only poster, and a schedule delivered as a spreadsheet or a database export can be maintained. Structure means one row per cable with consistent columns, keyed to a location reference that also appears on the drawings and the labels. Reconciliation means the schedule describes what was installed rather than what was designed, with every deviation listed and dispositioned.
Those three requirements cost almost nothing to state, and they change the value of the document set completely. A reconciled, editable schedule is the starting point for every future change and the basis for condition assessment. A scanned schedule leaves the next engineer to rebuild the data before they can use it, and the first thing that gets rebuilt incorrectly is the part nobody checked.
Two further records sit alongside the schedule. The first is the as-built drawing set, which should show the routes as installed, including the capacity that was reserved and not used. That reserved capacity is the most valuable information in the handover documentation for a hall that will grow, and it is invisible on a design drawing that predates installation. The second is the test record set, which has to stay linked to the schedule so that a circuit reference in a test record points to the same cable as the same reference in the schedule. Our note on data center cabling checklist for EPC projects sets out how the pieces fit together, and the evidence expectations of an audit are covered under TIA-942 certification testing.
Naming Conventions: The Cheap Decision That Saves Weeks
A naming convention is a document that costs an afternoon and prevents a category of error that costs weeks.
The convention has to satisfy three tests. It has to be unique, so that no two cables share a reference. It has to be derivable, so that a person standing in the hall with a drawing can work out what a cable should be called without looking it up. And it has to be stable, so that a reference does not change when something else in the building changes.
Most conventions that fail, fail on the third test. A reference that embeds the equipment it currently connects to becomes wrong the first time that equipment is replaced or its position changes in the numbering scheme, and correcting it means relabeling both ends of every affected cable. A reference based on position and function, with the connection details held in the schedule rather than in the label, survives those changes.
The convention also has to cover the label content, not only the cable reference: which position carries which information. Both ends typically carry the cable reference; penetration labels usually add the compartment reference because that is what the fire stopping register uses; tray exit labels often carry the route reference. Getting that mapping written down before installation is what turns labeling from a site judgement into a task. The interface with the penetration register is covered in our note on firestop cable penetration systems, and the vertical route labels belong to the same scheme, as set out in our note on procuring riser cable.
What to Freeze Before Handover
| Item | What to State | Evidence to Attach | Cost of Leaving It Open |
|---|---|---|---|
| Naming convention | The reference format, its uniqueness rule, and the label content at each position | Convention document issued before installation starts | Duplicate or unstable references, and relabeling of both ends of affected cables |
| Label material and print method | Thermal transfer printing, the ribbon, and the sleeve or marker material for each location class | Approved sample label per class, with the material datasheet | Faded or detached labels within a few years, and physical tracing of circuits |
| Position rule | Both ends, each penetration, each tray entry and exit, and interval rules on long runs | Label count per cable as a calculated quantity, not an estimate | One-end identification, which is half identification at a fraction of the saving |
| Sheath legend request | What the cable supplier can print along the sheath, and whether a project reference can be included | Written confirmation before the order is placed | Site labeling labour that the factory could have absorbed at almost no cost |
| Printer data retention | That the label printer's data file is handed over, not only the printed labels | Data file in editable form, with the naming convention referenced | Every future label made by hand, because nobody kept the source data |
| Schedule format | Editable spreadsheet or database export, one row per cable, columns defined | Delivered file plus a documented column definition | A poster rather than a working document, and the data rebuilt by the next engineer |
| As-built reconciliation | That the schedule and drawings describe what was installed, with deviations listed | Reconciliation record with each deviation dispositioned | A handover set that contradicts the installation, and tracing work to find out which is right |
| Reserved capacity record | The spare routes, tray fill and riser capacity left available, marked on the as-built drawings | Annotated as-built drawings plus a capacity statement | The most valuable information for expansion, lost at the moment of handover |
When Premium Labels Are Not the Answer
Durable identification is cheap insurance on permanent circuits, and there are places where it is not the right purchase.
Temporary works and construction power. Labels applied to temporary distribution are removed with the installation. Standard stock labels are the correct answer, and spending on sleeves for cable that will be recovered is waste.
Patch cords and frequently changed connections. Where connections change regularly, the identification that matters is the port, not the cable, and it belongs to the panel schedule rather than to a label on a cord. Labelling cords elaborately creates a maintenance obligation that nobody will meet.
Where the register will not be maintained. A coded label linked to an asset register only pays back if the register is kept current. Buying the code format without the maintenance process produces scans that return records which no longer match the installation, which is a worse position than a simple label, because it produces confident wrong answers. Where there is no asset management process, buy the durable label and the editable schedule, and leave the coding for when the process exists.
Where the real problem is that nothing is recorded. Some projects buy premium identification to compensate for the absence of a schedule. The schedule is the cheaper and more valuable item, and it should come first. What the verification of these records looks like is covered in our note on grounding and bonding verification, where the same bonding schedule discipline applies.
RFQ Checklist
- Naming convention document, issued before installation, with the uniqueness and stability rules stated
- Label content per position: both ends, penetrations, tray entries and exits, interval markings
- Print method specified as thermal transfer, with the ribbon type named
- Label material per location class, with a sample approved before the bulk order
- Adhesive versus sleeve decision per location, with sleeves required where the environment is hostile
- Sheath legend requirement confirmed with the cable supplier before the order is placed
- Label count per cable calculated from the position rule, priced per cable rather than as an allowance
- Printer data file handed over in editable form, not only the printed output
- Cable schedule in spreadsheet or database form, one row per cable, with column definitions documented
- As-built drawings showing installed routes, reserved capacity and spare tray fill
- Test records and penetration register linked by the same cable references used in the schedule
- Confirmation that the schedule was reconciled to the installation, with deviations listed and closed
Conclusion
Identification and documentation are bought as labour and delivered as a schedule, and the two specification decisions that matter most are the position rule and the file format. A label at one end is half a label; a schedule delivered as a scan is a poster. Add a naming convention agreed before installation, a sheath legend requested before the cable is made, and an as-built record that marks the capacity left for the next phase, and the handover set becomes the working document for the life of the hall.
Kexingyu Cable Group (KXYE) supplies the cable that these schedules describe, including the WDZ-YJY, WDZN-YJY, BTTZ, BBTRZ, NG-A (BTLY), KVV and YJV ranges and the multi-purpose distribution cable used on submain routes, all from one factory group with copper price linkage available on project-scale orders. Sheath legends are set at manufacture, so tell us at enquiry stage what reference format you want printed along the cable and we will confirm what can be included. Send your circuit schedule format and the identification convention you intend to use, and we will return cable data that fits it; the fastest route is a request for quotation.


