
Buying Connector Contacts and Plating for Vibration Duty: What to Specify and What It Costs
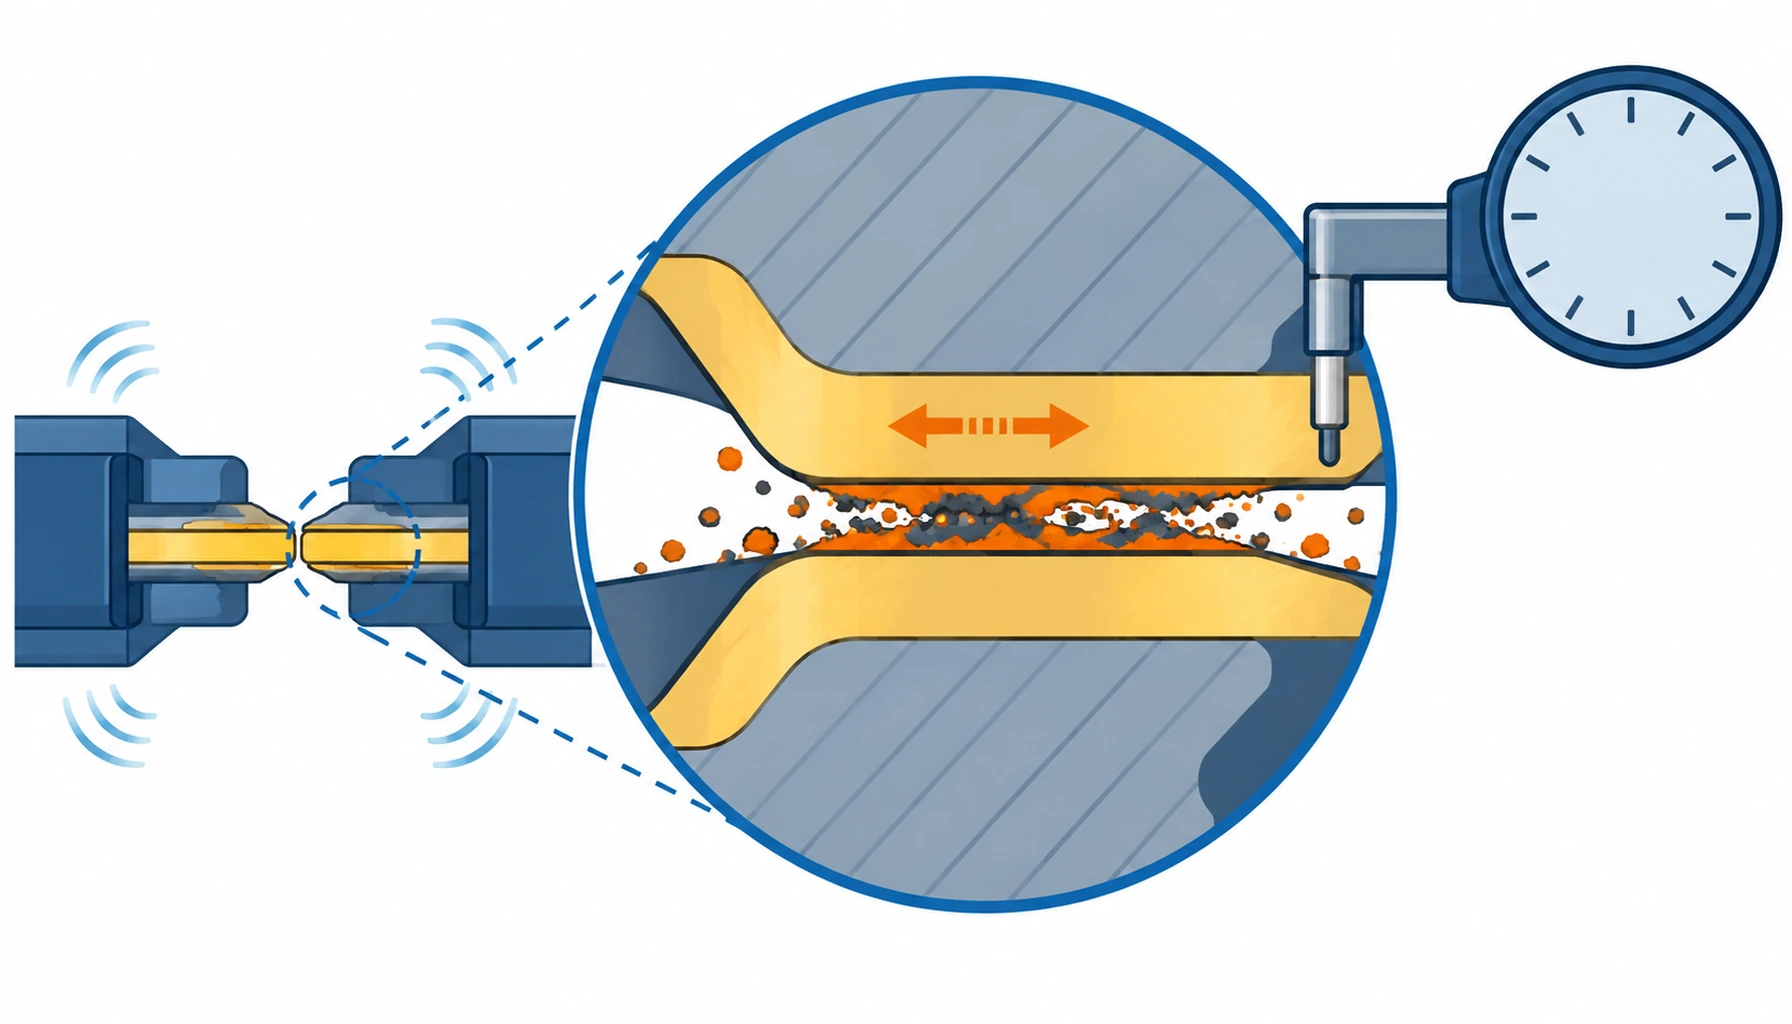
Quick Answer: Two decisions sit inside every contact: the base metal and the plating. The base metal carries the current and the spring force; the plating decides what happens at the interface when the machine vibrates. On any moving axis, a gold over nickel system resists the small sliding motion that corrodes tin, while plain tin contacts can read perfectly on the bench and go open months later. Specify the plating type, its thickness and its underplate, and put the mating cycle number next to them, because which plating is right depends on how often the joint is disturbed.
Introduction
Contact plating does not appear on most connector drawings at all. Buyers specify the housing, the pin count, the current and the IP class, and the plating is whatever the catalogue happens to list. That is a reasonable shortcut in a cabinet, where contacts are mated once and left alone. It is a poor shortcut on a robot axis, where the joint is in constant small motion and the plating is exactly what decides whether the signal stays stable for years or drifts out within months.
The harness overview in our note on robot harnesses and connectors places the contact among the other elements of an assembly. This guide stays on the contact itself: why vibration punishes some plating systems and not others, and what to write into the order so the system you need is the one you get.
Base Metal and Plating Are Two Different Decisions
The base metal for most signal and power contacts is a copper alloy chosen for conductivity and spring properties. Its job is to carry the current and hold the normal force that presses the two halves together, and the spring force matters as much as the plating, because a contact that has relaxed cannot be saved by any surface treatment.
The plating is a system, not a single layer. It is usually a thin underplate, most often nickel, that stops the base metal and the top layer from interacting, with a functional top layer doing the actual work. Getting the underplate wrong causes its own failures: too thin and the base metal diffuses through, too thick and the layer can crack under the same vibration it was meant to survive. So the specification line is three numbers, not one, and that is the first thing to fix in the RFQ.
Why Vibration Changes the Answer
Vibration does something specific to a mated contact. However tight the fit, the two surfaces move against each other by a few micrometres each cycle, and that small sliding motion is enough to break and reform the metal-to-metal boundaries at the interface. On gold, the metal stays metal and the contact resistance barely moves. On tin, each movement exposes fresh metal that oxidises within minutes, and the oxide is an insulator that builds up at the contact area until the joint goes intermittent and finally open. That process is fretting corrosion, and it is the single most common reason a connector that passed every bench test fails in the field.
Two variables decide how fast it happens: how far the surfaces slide, and how many times they do it. A connector on a fast axis with a high cycle rate is the worst case, and it is exactly where the cheaper plating fails first.
The Decision Table: Plating Systems and Where Each Belongs
| System | Where It Belongs | What to Specify | Evidence to Demand | Where It Fails in Service |
|---|---|---|---|---|
| Hard gold over nickel | Moving axes, high-cycle joints and low-level signal contacts | Gold thickness in microinches or micrometres, hardness, nickel underplate thickness | Plating thickness certificate and a fretting or vibration test result | Underplated or too-thin gold worn through to the nickel, raising resistance at the edge of the contact |
| Gold flash | Static cabinet contacts and joints mated once | That it is flash, not functional gold, and the duty it is approved for | A plating certificate stating the actual thickness | Flash worn away after a handful of mates, leaving bare base metal on a joint thought to be gold |
| Tin | Static power terminals and connectors never disturbed in service | A no-motion clause, plus a mating cycle limit, since tin is not a vibration surface | Confirmation of the duty, and a vibration qualification if the route moves at all | Fretting corrosion that reads fine at the bench and opens within months on a moving axis |
| Silver | High-current contacts and power joints where resistance must stay low | Silver thickness, a tarnish or sulphidation control, and the mated environment | Contact resistance evidence and a tarnish test where the atmosphere is aggressive | Tarnish under sulphur-bearing air, raising resistance slowly enough to go unnoticed |
| Selective plating | Contacts where gold is needed only at the mating area | Where the gold applies, its thickness at the contact zone, and the base metal elsewhere | A drawing showing the plated zone and a sectioned sample | Gold placed narrowly, so the wipe track leaves the plated zone during mating |
Thickness, Porosity and Mating Cycles
Thickness on its own does not settle the question; what settles it is thickness over the right underplate, tested for porosity. A gold layer that looks generous on a certificate can still be porous, and pores are where the underlying nickel and the base metal corrode through the gold. For a contact on a moving axis, the gold thickness needed is higher than for a static joint, and the specification should name it as a minimum at the contact area rather than as an average over the whole part.
Mating cycles belong next to the thickness because they wear the plating away. A tool changer that mates hundreds of times a day is a different problem from a motor joint mated once at build: the first needs a plating and a contact geometry rated for the cycle count, the second can accept a lighter surface. Write the expected cycle count into the order and ask for the contact rating against it; our note on why robot connectors fail shows how plating wear and fretting appear together in a failed part, and the entry mechanics that take some of the motion out of the joint are covered in our note on terminating robot harnesses.
What to Freeze Before the Order
| Item | What to State | Evidence to Attach | Cost of Leaving It Open |
|---|---|---|---|
| Base metal alloy | The copper alloy and its spring properties for the contact size | Material datasheet naming the alloy and the normal force | A contact that relaxes and loses force, which no plating can recover |
| Plating system | The top layer and the underplate, named as a system rather than one word | A plating specification with both layers and their thicknesses | A catalogue default that is wrong for the vibration duty |
| Gold thickness at the contact area | A minimum at the mating zone, not an average over the part | A thickness certificate and a porosity test | Plating worn through to the underplate at the wipe track |
| Underplate thickness | Nickel or equivalent, with the thickness and its function stated | A sectioned sample showing the layer structure | Diffusion through a thin underplate, raising resistance over time |
| Mating cycle count | The cycles the joint will see, and the contact rating against that number | The contact maker's rating for the stated duty | Plating worn out in months on a high-cycle tool changer |
| Contact normal force | Minimum force at the contact, and how it is maintained over the temperature range | A force measurement on the finished contact | Fretting driven by a joint that is not tight enough to resist motion |
| Environment and tarnish | Atmosphere and any sulphur or chemical exposure, for silver and bare copper | A tarnish or corrosion test where the duty requires it | A slow resistance rise that only appears in the field, not at the bench |
| Plated zone drawing | Exactly where the functional plating applies on the contact | A dimensioned drawing and a sectioned sample | Gold placed narrowly, so the mating wipe leaves the plated area |
When Gold Is Not the Answer
Where the joint never moves. Static cabinet terminals and screw connections do not need gold, and paying for a vibration-grade plating on a contact that is mated once is spend that never returns. Match the plating to the motion: functional gold on the axes, a lighter surface in the cabinet.
Where the fault is force, not surface. If a contact has relaxed and is no longer pressing hard enough, the cleanest way to stop the small sliding motion is a spring rating that suits the duty, not a thicker plating. Plating resists the damage; normal force prevents it.
Where the joint is not actually tight. A connector with too much free play will move whatever the plating, so the mechanical fix, a better entry and a correctly seated contact, has to come first. The entry itself is judged separately in our note on the strain relief at the connector interface.
Where the sealing is being forgotten. Plating protects against fretting; it does nothing about contamination, and a gold contact in a connector that lets water and dust reach the interface will still fail. Ingress conditions are judged on their own in our note on IP ratings for robot connectors. Where the same joint also has to hold a screen at the shell, the plating and the EMC bond are two separate requirements, which our notes on M8 and M12 connectors and on heavy-duty rectangular connectors set out for their families.
RFQ Checklist
- Base metal alloy named, with the spring properties and normal force for the contact size
- Plating named as a system: top layer plus underplate, with both thicknesses stated
- Gold thickness given as a minimum at the mating zone, not as an average over the part
- Underplate thickness stated, with its function, and a sectioned sample to prove the layer structure
- Mating cycle count written into the order, with the contact rating against that number
- Minimum contact normal force specified and measured on the finished contact
- Porosity test required on the plated surface, not only a thickness certificate
- Plated zone shown on a dimensioned drawing, so the wipe track stays inside it
- Environment and tarnish exposure stated where silver or bare copper is used
- Vibration or fretting qualification required for any contact on a moving axis
Conclusion
Plating is the cheapest line on a connector drawing and one of the most expensive to get wrong, because the failure it causes is intermittent and slow. On anything that moves, specify the plating as a system, put a thickness on the mating zone, name the mating cycles, and ask for the porosity and vibration evidence that shows the surface will survive the duty. On anything that does not move, do not pay for the vibration grade.
Kexingyu Cable Group (KXYE) supplies the cable side of these joints: the continuous flex and screened constructions whose conductor stranding and screen geometry are designed to keep a contact stable through years of motion rather than load it with movement it cannot take. Send us the duty, the cycle count and the connector schedule, and we will return constructions and sample lengths that fit; the fastest route is a request for quotation.


