
Power Equipment Sourcing for Middle East Infrastructure Projects
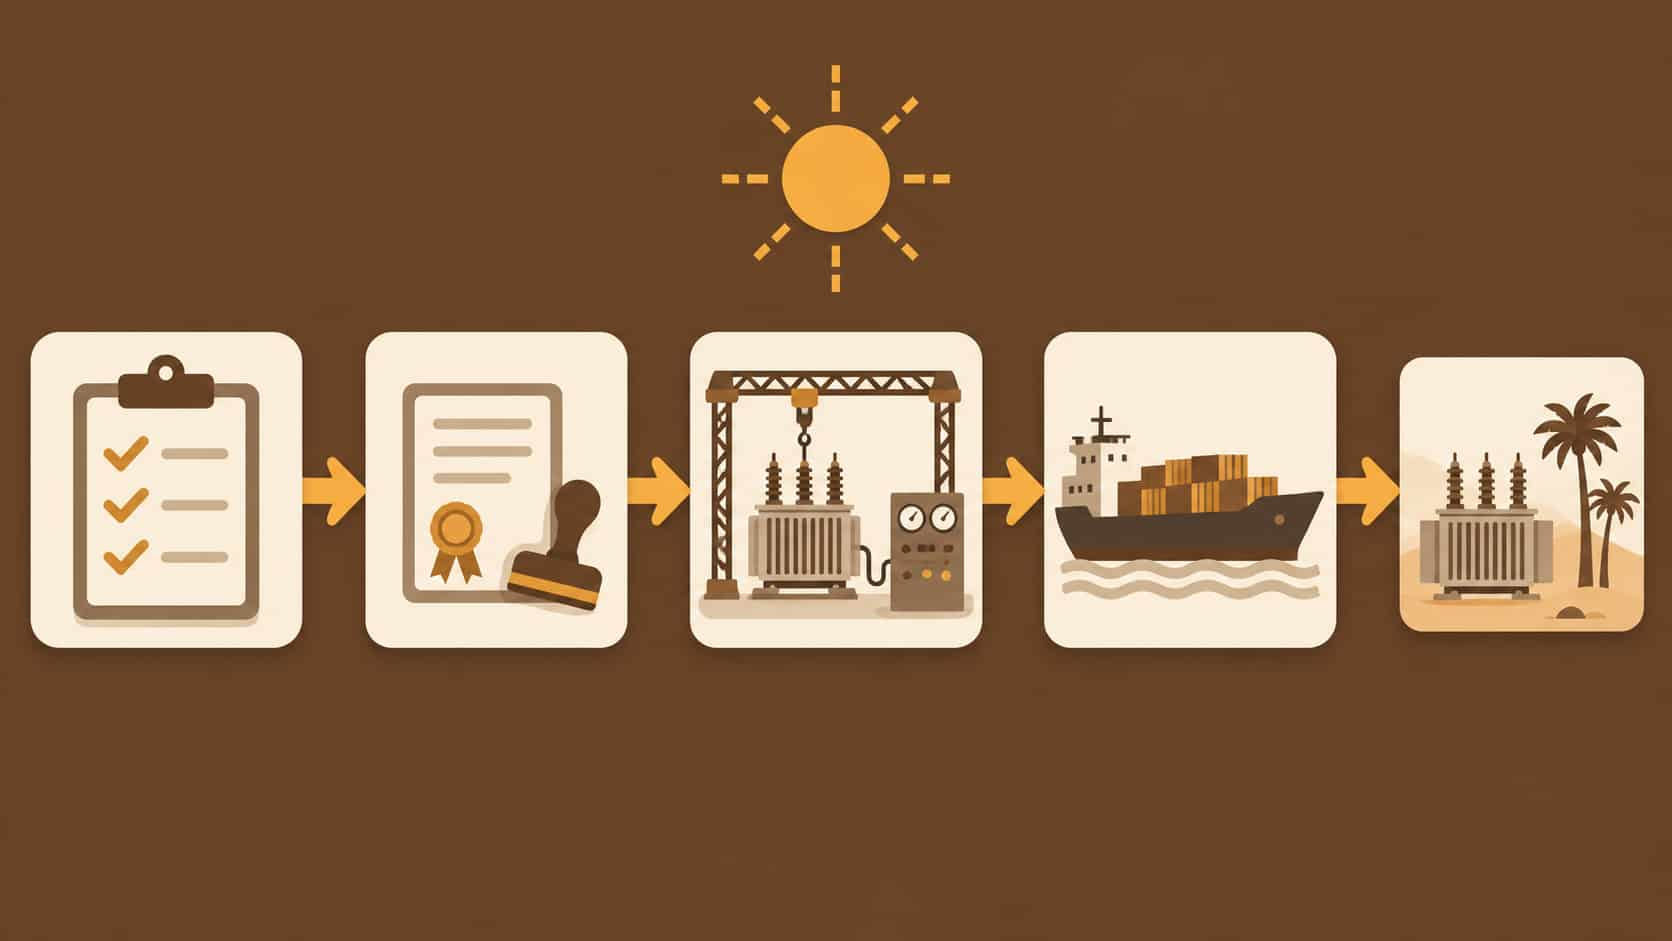
Between a Gulf megaproject's specification and its energisation stand three filters—desert-duty engineering, regional approvals and contract discipline—and equipment that clears all three is worth sourcing carefully.
Introduction
The Middle East is building power infrastructure at a scale few regions match: giga-projects and new cities, industrial cities fed at 132 kV and above, grid interconnection across borders, and a solar build-out that keeps redrawing the generation map. For buyers—developers, EPC contractors, government procurement arms—the equipment market is genuinely global, with manufacturers from Asia, Europe, Turkey and the region itself all bidding into the same tenders.
Sourcing well here is not about finding the cheapest nameplate. It is about matching equipment to desert reality, clearing the region’s approval gates before the order rather than after, and structuring contracts so that inspection, shipment and payment milestones reinforce each other instead of colliding. This guide walks through each filter in turn. The equipment fundamentals are covered in our transformers and substations resources; this article stays with the sourcing discipline that turns a specification into an energised project.
What Middle East Conditions Demand from Equipment
Regional conditions are not marketing adjectives; they are specification lines with numbers attached.
- Ambient temperature. Design ambients of 50 °C and above are standard across the Gulf. Transformers need heat-run data at the actual ambient, switchgear needs derated continuous currents verified at enclosure temperature, and generator sets must show output at site temperature and altitude—nameplate ratings at ISO conditions flatter every machine.
- Sand and dust. Fine, airborne dust penetrates enclosures and fouls cooling. IP ratings belong on every outdoor item, ventilation design matters as much as sealing, and filter maintenance access decides whether a cabinet ages gracefully or cooks its components.
- Coastal corrosion. From the Gulf coast to the Red Sea, salt-laden air attacks steel and aluminium. C5-class coatings, stainless fasteners and sealed enclosures are specification items, not options.
- Solar load on enclosures. Direct sun on outdoor cabinets adds decades of thermal ageing in a few years. Sunshields, reflective finishes and shaded siting belong in the layout from day one.
- Grid codes and utility standards. Each state utility maintains its own connection requirements—voltage ranges, frequency ride-through, protection philosophies and approved-vendor lists. Equipment compliant in IEC terms still needs mapping to the local standard before the design review, not after it.
The pattern across all five: the difference between equipment that survives and equipment that fails early in the region is rarely the nameplate—it is the environmental engineering around the nameplate.
Certifications and Approvals That Open the Door
Regional procurement runs on paperwork as much as performance, and the paperwork has layers. The base layer is IEC type testing—transformers to the IEC 60076 series, switchgear to the IEC 62271 series—witnessed or documented by accredited laboratories. The second layer is national conformity: Saudi Arabia’s SASO regime and its quality-mark requirements, the approval schemes of state utilities such as DEWA in Dubai and Kahramaa in Qatar, and the assorted national standards bodies that each maintain their own certificate lists. The third layer is project-specific: the engineer-of-record’s design review, the contractor’s submittal cycle and, on giga-projects, the client’s own vendor qualification process.
The sourcing rule that saves months: map the approval path before shortlisting suppliers. A manufacturer with an excellent product but no SASO file, no witnessed-test history in the region and no local reference will spend your construction window learning the system. Ask every bidder for their approval inventory for the specific state you are building in—certificates by number, references by project—and treat hesitation as information.
Specifying for Desert Duty
The table condenses the specification points that separate region-ready equipment from catalogue-standard product, block by block.
| Equipment | Regional Duty Demands | Specify at Order Stage |
|---|---|---|
| Power and distribution transformers | 50 °C ambients, solar gain, dust on coolers | Heat-run data at site ambient; oversized or filtered cooling; C5 coating class; bushings and conservator seals rated for thermal cycling; losses priced into evaluationâour transformer sizing guide covers the rating logic |
| MV switchgear and RMUs | Dust ingress, enclosure heating, condensation at night | IP-rated outdoor variants with filtered ventilation; continuous current verified at enclosure temperature; internal-arc classification; anti-condensation heaters as standard |
| Generator sets | Derating at temperature, sand-laden intake air | Output stated at site conditions, not ISO; heavy-duty air filtration; oversized radiators; fuel systems sealed against contamination |
| Solar-hybrid and storage systems | Extreme cell and battery temperatures | Battery thermal management rated for site ambient with margin; container insulation and sunshields; inverter derating curves documented |
| Cables and accessories | Soil temperatures, termitic and rodent exposure, salt marsh | Cable rated for ground temperature at burial depth; rodent-resistant sheaths where specified; joints and terminations from one matched system |
One cross-cutting note: factory acceptance testing should simulate regional duty, not just standard points. A witnessed FAT that runs the heat-run at site ambient, verifies enclosure temperatures under load and demonstrates filtration performance catches exactly the failures that field experience predicts. Our article on why FAT matters for switchgear details the witness-test logic; insist on the regional-duty version of it.
The Sourcing Route: Manufacturer Direct, Agent or EPC Package
Three routes dominate regional sourcing, each with a fit. Manufacturer direct maximises price and technical access, and suits buyers with engineering staff to manage submittals, inspections and logistics. Local agents and distributors carry the approval files, stock fast-moving items, and speak the utility’s language—valuable where schedules compress and approvals gate progress. EPC-packaged supply moves the interface risk to the contractor: one scope, one warranty, one throat to choke, at the cost of visibility into equipment selection. Hybrid arrangements are common—major transformers direct from the manufacturer, balance-of-plant through a regional agent, packaged substations as factory-integrated units. Our article on prefabricated substations explains when factory integration beats field assembly in schedule-sensitive projects. And for the growing share of remote infrastructure that pairs generation with storage, our guide to generator-storage hybrid systems covers the control integration those packages need.
Whichever route, keep two disciplines. First, name the responsible engineer for each approval on each side—an approval that belongs to nobody misses its window. Second, freeze the environmental specification early: desert-duty requirements negotiated after the order arrive as change orders priced accordingly.
Contracts, Inspection and Shipment
Regional projects typically run on FIDIC-family contracts with engineers’ approvals gating payment, and equipment orders sit inside that structure. Three contractual mechanics decide most sourcing outcomes: the letter of credit and its deadlines, which reward suppliers who treat documentation as a deliverable and punish those who discover discrepancies at the bank; third-party inspection—SGS, Bureau Veritas or the client’s inspector—witnessing FAT and issuing the certificates that release payment; and pre-shipment and arrival inspection, which allocates damage risk at the correct boundary. The table lists the failure modes and the contractual countermeasures.
| Risk | How It Bites | Countermeasure |
|---|---|---|
| Approval delays stall energisation | Equipment arrives compliant with IEC but missing the state utility's file; design review reopens | Approval inventory per state verified at bid stage; submittal schedule with named approvers; milestone payments tied to approval progress, not shipment alone |
| Letter-of-credit discrepancies | Shipment completes but documents bounce at the bank; payment freezes for weeks | Document checklist agreed with the issuing bank before order; supplier references with clean LC history; pre-shipment document review by both parties |
| FAT quality gap | Tests pass at standard points but fail regional duty in the field | Witnessed FAT at site ambient and enclosure temperatures; third-party inspector named; regional-duty acceptance criteria written into the order |
| Lead-time drift on critical items | Transformer slot slips a quarter; the construction season is lost | Factory slot reservation at order with liquidated dates; phased deliveries; approved alternatives for the critical path named in advance |
| Spares and support vacuum | Years one to five pass; the agent who quoted is gone; parts come from nowhere | Commissioning spares per lot; regional spares stocking commitment in writing; service response times with named regional partners |
When the Lowest Bid Is Not the Deal
Regional tendering rewards price discipline, but three situations convert the lowest bid into the most expensive outcome: a bid that quietly assumes standard-duty equipment (the derating and coatings reappear as variations); a bid without the state’s approval file (the approvals delay lands on your programme); and a bid without regional service capability (year-three parts arrive by air freight at buyer’s cost). Evaluating on total delivered, approved and supported cost—rather than CIF price alone—ranks suppliers the way the project will actually experience them.
Conclusion
Sourcing power equipment for Middle East infrastructure is a three-filter exercise: engineer for the desert, clear the approvals, contract for the journey. Equipment specified at 50 °C ambients with C5 coatings and filtered ventilation, bought from suppliers whose approval files already exist, under contracts that tie inspection, shipment and payment into one coherent sequence, arrives on site and stays energised.
The suppliers who belong on your shortlist are the ones whose first questions are about your site ambient, your state utility and your LC terms—because those three answers, more than any catalogue, determine whether the deal works. Buyers who ask the same questions back get equipment that passes its FAT the first time and its summers for the next twenty years.
Frequently Asked Questions
Short answers to the questions buyers ask about sourcing power equipment for the region.
Recent Posts
Voltage Stabilizers vs UPS: Do You Need Both?
Voltage Stabilizers vs UPS: Do You Need Both? One device fixes how high or low the voltage is; the other fixes whether there is voltage
Energy Storage for Data Centers: A Growing Backup Power Option
Energy Storage for Data Centers: A Growing Backup Power Option Batteries have always backed up data centers in the form of UPS strings. Grid-scale BESS
Thermal Runaway in Lithium Batteries: What BESS Buyers Should Understand
Thermal Runaway in Lithium Batteries: What BESS Buyers Should Understand How thermal runaway starts, how it propagates, and which evidence buyers should require before approving