
Prefabricated Modular Cabling: Building Data Centers Faster
Quick Answer: Prefabricated modular cabling moves cable cutting, termination and testing into the factory, ships complete power and network assemblies to site, and turns a data hall into a plug-and-commission exercise — trading on-site labor for design freeze.
Introduction
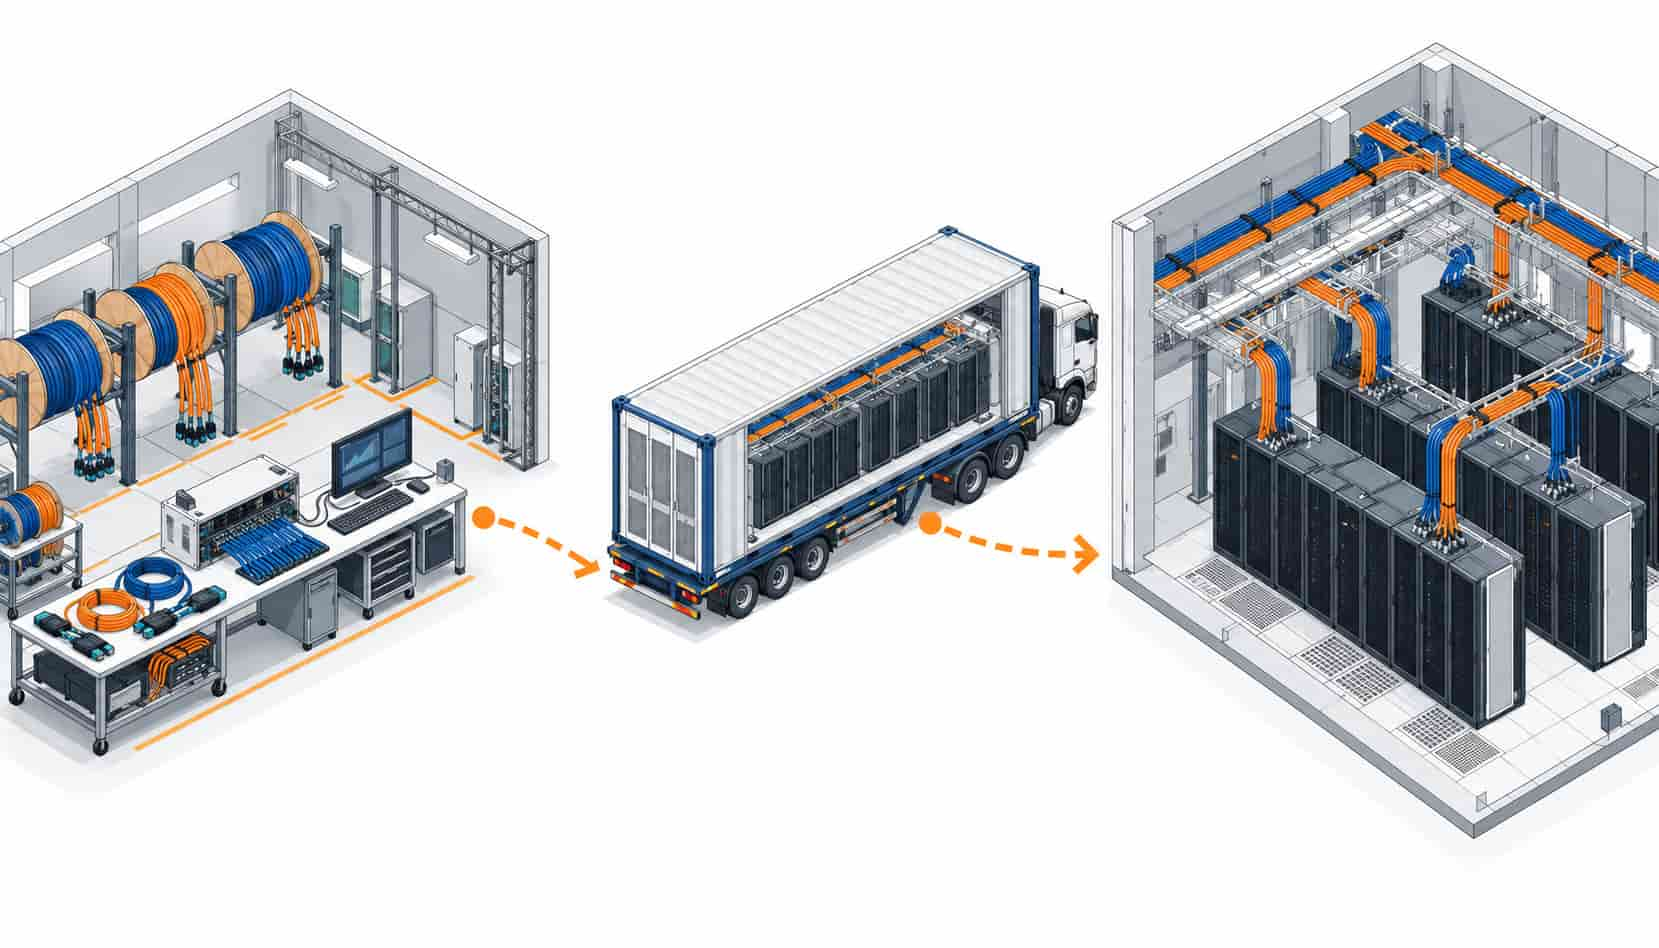
Traditional cable installation front-loads its risk to the site: conductors cut on the floor, terminations made on ladders, quality proven only when the circuit is energized. Prefabrication reverses the sequence. Assemblies are built on benches with calibrated tooling, tested before they ship, and installed by connection rather than fabrication. The approach is not new — pre-terminated fiber and factory-built switchgear skids have coexisted for years — but AI-era schedules have pushed it from preference to strategy, because the schedule itself has become the constraint as data center power demand accelerates.
The equipment side has already industrialized this logic: containerized and skid-mounted solutions are mainstream in power infrastructure, from prefabricated substations to fully integrated modular data center products that ship as finished rooms with power, cooling and cabling installed. Those integrated halls — of the kind pioneered in China’s modular data center market, where a containerized hall arrives with racks, busway, cabling and monitoring factory-fitted and the site work reduces to connecting power and network — set the benchmark this article borrows for cable-specific prefabrication.
What Prefabrication Actually Changes About Cable
Three things change, and each one moves risk from site to factory. First, geometry: cable lengths are calculated from drawings and cut on calibrated lines, which eliminates the on-site guesswork that produces both slack coils behind cabinets and mid-run joints where a drum ran out. Second, terminations: lugs are crimped with documented tooling by assemblers who repeat the same joint hundreds of times, and every set is routine-tested — conductor resistance and withstand — before packing. Third, verification: a factory assembly arrives with a test certificate per circuit, so commissioning starts from evidence instead of generating it under schedule pressure.
The site consequence is a different labor profile. Instead of electricians pulling and terminating for weeks, the hall hosts installation crews connecting labeled assemblies to labeled positions — a task measured in days per hall, with punch lists that shrink because the error-prone work never happened on site. Project teams that track cost by schedule risk, not just by line-item price, usually find the premium for prefabrication repaid before the first audit.
The Power Side: Skids, Busway and Feeder Assemblies
Power prefabrication starts with the skid: switchgear, transformers and UPS modules mounted and wired at the factory, with internal cabling loomed, labeled and tested as part of the equipment package — the same discipline detailed in planning around switchgear lead times, where factory-integrated delivery shortens the critical path. The logic extends across the supply chain squeeze that AI-era building has produced, from switchgear to transformer shortages and their lead-time consequences: anything that moves verification into the factory also buys schedule certainty that procurement alone cannot. Between skids and to the halls, prefabricated feeder assemblies replace field-cut cable: factory-terminated single-core sets on drums with pulling eyes, or pre-cut multi-core assemblies with both ends terminated and tagged to the cable schedule.
Inside the hall, busway completes the method. Tap-off boxes plug into an overhead bus route in minutes, and row-level capacity changes by swapping a breaker module rather than re-pulling cable — which is why modular and AI halls lean on busway for the last distribution hop and reserve prefabricated feeders for the fixed backbone. The cable supplier’s role concentrates where flexibility is real: the long MV and LV feeders between intake, skids and halls, cut to measured route lengths with factory-tested terminations, delivered on a schedule matched to the installation sequence.
The Network Side: Pre-Terminated Trunks and Backbone
Structured cabling adopted prefabrication earlier and more completely than power. Pre-terminated copper trunks and MPO fiber assemblies arrive with tested polarity, labeled ports and guaranteed channel performance — moving the link budget from a site hope to a factory measurement. The hall cabling then becomes a plug-in exercise: cassette panels receive trunks, patch cords finish the circuit, and moves-adds-changes happen at the panel for the life of the hall.
The specification language changes accordingly. Instead of buying bulk cable and field terminations, the buyer schedules assemblies: trunk length, port counts, breakout configuration and test data per assembly. Quality shifts from workmanship inspection to document review — the assembly certificate and measured insertion loss replace the punch-list check — and the conductor-material traps of bulk copper purchasing, covered in the structured cabling guides, apply at the factory audit level rather than the drum level.
| Aspect | Traditional Field Installation | Prefabricated Modular |
|---|---|---|
| Cable lengths | Measured and cut on site; slack coils and mid-run joints are common | Cut to schedule on factory lines; route-accurate, joint-free critical runs |
| Terminations | Made on ladders under schedule pressure; quality varies by crew | Crimped with calibrated tooling by production staff; torque and die records kept |
| Testing | First full test at commissioning, when rework is most expensive | Routine test per circuit before shipping; commissioning starts from evidence |
| Site labor profile | Weeks of pulling and terminating electricians | Days of labeled connection work; smaller, faster crews |
| Schedule risk | Accumulates on site: access, sequencing, rework | Concentrates before shipping: design freeze and factory slot must hold |
| Change response | Flexible late; lengths adjusted as routes move | Costly after release; changes route through factory re-planning |
| Best fit | Renovations, ambiguous routes, one-off rooms | Repeatable halls, tight schedules, constrained sites, multi-campus programs |
Containerized Halls: Prefabrication Taken to the Building
At the far end of the spectrum sits the containerized modular data center: a complete hall built in a factory frame, with racks, busway, cabling, cooling and monitoring installed and tested before it ships. Integrated products of this type — such as the containerized halls from established Chinese modular data center vendors, which arrive IP-rated for outdoor placement, operational across extreme ambient ranges and positioned so that site work reduces to power and network entry — compress the commissioning curve to weeks. The cable scope inside them is a demonstration of everything this article describes: loomed and labeled power feeders, factory-terminated network trunks, and a test file that travels with the hall.
Buyers who operate between the two extremes — fully containerized on one end, fully field-built on the other — get the best economics by mixing: containerized or skid-based blocks for the standardized core, and prefabricated feeder and trunk assemblies for the campus links between them. The mixing rule is simple: prefabricate what repeats, field-build what is unique, and make the cable schedule say which is which.
The Design Freeze Trade-Off
Prefabrication’s constraint is the mirror of its speed: the design must be frozen early enough for the factory to build, and late enough to be right. Route lengths, rack positions, port counts and skid placements all move from site decisions to drawing decisions, which reshapes project governance — coordinated drawings, clash detection and measured route surveys happen before the order releases, not as site improvisations. Programs that already run disciplined design phases absorb this easily; programs used to fixing routes on the fly need to change their rhythm, not their tooling.
The commercial protection is staged release. Cable schedules are prefabricated in lots matched to the installation sequence, so a late route change affects the unreleased lot rather than the whole order. A manufacturer set up for project-scale supply holds the drums, assembly capacity and documentation flow to work that way — the production depth that separates factories from intermediaries, which our checklist on telling a cable manufacturer from a trading company turns into concrete questions — and quotes against a copper price linkage so the metal basis agreed at release holds through each lot’s delivery, which keeps the freeze honest commercially as well as technically.
| Cable Scope | Prefab Readiness | How to Order It |
|---|---|---|
| MV feeders intake to skids | High, once routes are surveyed | Factory-terminated single-core sets cut to measured routes, drums sequenced per lot |
| LV feeders skids to halls | High for repeatable hall layouts | Pre-terminated or eyelet-terminated assemblies, tagged to the cable schedule |
| UPS and battery room cabling | Medium; room conditions vary | Cut-to-length Class 5 assemblies with factory lugs; field connection at cabinets |
| Hall distribution | Busway led; cable minimal | Bus route plus tap-off modules from the busway vendor; feeds prefab to the riser |
| Structured cabling backbone and horizontal | Very high â mature method | Pre-terminated MPO fiber trunks and copper assemblies with per-channel test data |
| Life-safety and fire circuits | Medium; authority rules vary by market | Prefab lengths where permitted; fire-stop and inspection points kept field-verified |
When Prefabricated Modular Cabling Is Not the Answer
The first honest exception is the project that cannot freeze. Renovations inside live facilities, sites with undefined routes, and owner changes that arrive weekly all defeat factory sequencing — the rework costs of prefab assemblies returned or re-cut exceed the site labor they were meant to save. The second is the small one-off build: a single edge room with a handful of routes gains little from factory tooling and pays the coordination overhead anyway.
The third exception is partial: even committed prefab programs keep certain scopes field-built, notably fire-stopping, final connections inside energized areas and anything the authority requires to witness on site. The discipline is scope honesty. Prefabrication is a scheduling instrument, not an ideology; applied to the wrong scope it manufactures rework at factory prices.
RFQ Checklist: Buying Prefabricated Cable Assemblies
- Measured route lengths per assembly, from coordinated drawings, with the survey method stated
- Assembly schedule: construction, cross-section, termination types and labels per circuit
- Lot split matched to the installation sequence, with per-lot delivery windows
- Factory test scope per assembly: conductor resistance, withstand, and continuity records
- Network assemblies: port maps, polarity, and per-channel insertion loss data
- Packing and transport plan: drum sizes, protection, and site offloading sequence
- Change procedure: how late route changes re-enter the factory plan and what they cost
- Standards and editions per assembly, as for conventional supply
- Documentation package: per-circuit certificates batched per lot, plus type test reports
- Pricing basis: copper price linkage per lot, validity across the program
Point that checklist at a factory that builds to schedule rather than to stock, and the prefabricated method delivers what it promises: a hall that commissions on the strength of documents that were finished before the trucks arrived.
Conclusion
Prefabricated modular cabling moves cable’s hardest work into the factory — cutting, terminating and testing — and moves its proof there too. The site becomes a connection exercise measured in days, the punch list shrinks to what was never prefabricated, and the schedule risk concentrates where it can be managed: in a design freeze backed by measured routes and staged lots.
For buyers assembling modular programs, the practical move is to qualify a cable partner that can quote, build and certify per assembly and per lot. Kexingyu Cable Group (KXYE) supplies route-cut, factory-terminated power and control assemblies alongside its conventional drum supply, with per-lot documentation and copper price linkage across the program. Send the coordinated drawings and the lot plan, and we will return an assembly-level offer.


