
How to Vet a Chinese Electrical Equipment Manufacturer Before Ordering
The quotation tells you what a factory wants to sell you. The vetting tells you whether the same factory can actually build it, test it and stand behind it two years later.
Introduction
China’s electrical equipment industry contains world-class manufacturers, competent mid-tier factories, and trading companies with impressive brochures and no winding machines. From outside, the three look similar: professional quotations, fluent English, certificates attached. The differences surface only later—as inconsistent test data at FAT, as a delivery that slips because a third factory is involved, as a warranty claim answered by silence. Vetting is how you see those differences while they are still cheap to see.
Vetting is not distrust; it is standard practice on both sides of the deal. Serious Chinese manufacturers expect it and are prepared for it—they keep guest routes through the workshop, test reports organized by contract, and reference projects willing to take a call. The friction usually comes from suppliers who would not survive the check, which is exactly the point of running it.
This guide gives the vetting framework working buyers use: six dimensions of due diligence, the remote checks to run before any flight, what to actually look at during an on-site audit, the verification methods compared, and the honest limits of a factory tour.
Why Vetting Beats Negotiation
Buyers often spend weeks negotiating price with a supplier they spent minutes qualifying. The economics are backwards. A five percent price win on a bad factory costs more than any discount returns: rework, schedule slip, retesting, and in the worst case a re-order from a second supplier while the project waits. Vetting, by contrast, is cheap—most of it can be done from a desk, and the on-site part costs one trip.
There is also a selection effect. Asking for evidence—certificates traced to source, reference projects, a workshop tour—filters the supply base before you invest negotiation effort in it. Factories that engage seriously with the process are telling you something about how they will behave when there is a problem at year two. Factories that dodge it are telling you something too.
The Six Dimensions of a Supplier
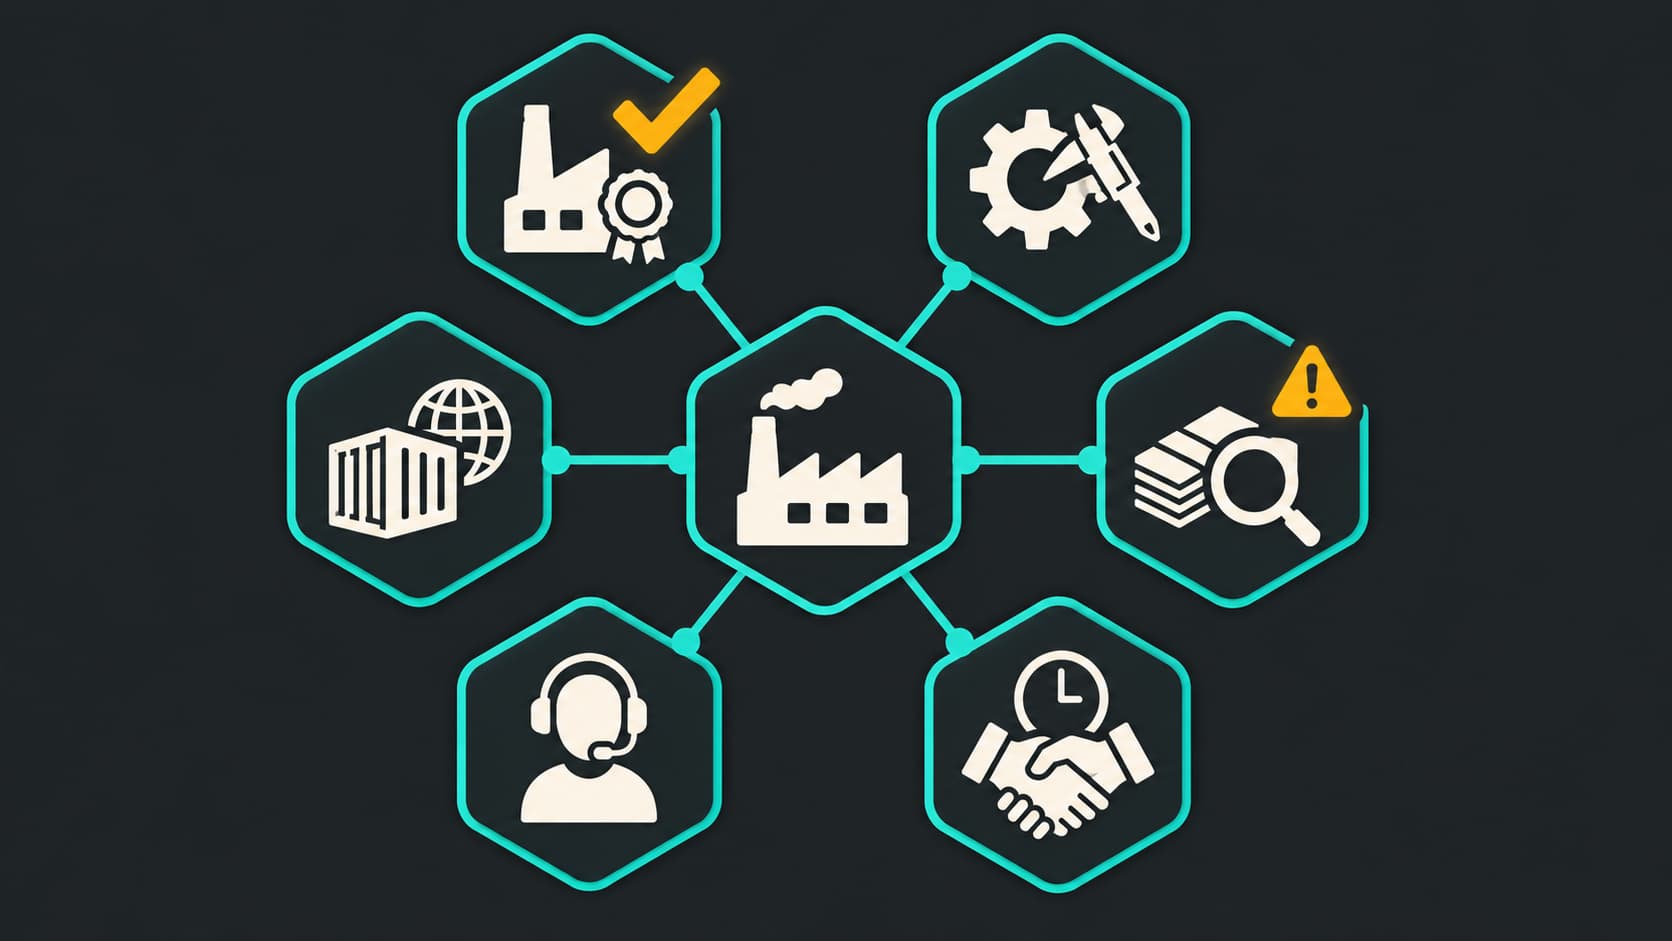
Due diligence on an equipment factory reduces to six dimensions. Different buyers weight them differently, but skipping one is how surprises happen.
| Dimension | What to Check | Red Flag |
|---|---|---|
| Legal entity and scope | Business license, registered capital, scope covering manufacturing (not just trade), years operating | Young entity with large claims; scope limited to trading; registered capital recently inflated |
| Production facility | Own workshops for the core processesâwinding, core stacking, tank fabrication, assembly, wiring | Photos that look like trade-show stands; core processes "handled by partners" |
| Test station capability | Own routine test sets and impulse or power-frequency labs for the product family | No test station on site; test reports all dated from other factories |
| Quality system in practice | ISO 9001 with scope matching the product; in-process inspection records; calibration logs | Certificate exists but workshop staff cannot describe the inspection flow |
| Export track record | Reference projects in your region or standard; customs data consistency; repeat customers | References that do not answer; export records that contradict claimed markets |
| Commercial stability | Ownership transparency, litigation checks, candid lead-time promises | Unwillingness to name beneficial owners; lead times dramatically better than the market |
The dimensions correlate. A factory that owns its winding shop almost always owns its test station; a factory that hides its ownership usually hides its subcontracting too. You are not checking six independent facts—you are building one coherent picture, and inconsistencies between dimensions are the strongest signal in the whole exercise.
Remote Checks Before You Book a Flight
Most vetting is desk work, and it eliminates most candidates. Start with the registry: business license, registered capital, scope of business, and how the numbers have moved over time. Verify certificates at their source—laboratories and certification bodies respond to written requests for confirmation, and the ones that do not respond resolve the question. Pull export data if your market’s records are accessible: a factory claiming West African project references with no export history there has told you something. Then hold a technical conversation that requires real knowledge—ask how their impulse test rig is configured, or what they do when a routine test value sits near the limit. The depth of the answer separates factories from resellers faster than any document.
The product-family guides on this site—our checklists for a Chinese transformer manufacturer, a Chinese switchgear manufacturer and a Chinese BESS manufacturer—carry the family-specific question lists this article stays general about, and the transformers and substations range overview maps where each product family sits in a project power train.
On-Site Audit: What to Actually Look At
An on-site audit is one to two days, and its value depends entirely on where you spend them. Skip the conference room. Ask to walk the material flow from raw material to dispatch, because that is where a real factory and a rented one look different. On the winding floor, check whether the machines match the capacity claims and whether work-in-progress carries travelers—job cards that name the contract, the operator and the inspection step. In the test area, look for the routine test sets and, for transformer families, the impulse generator: a factory without test capability is quoting equipment it cannot verify, and every test report it hands you was born somewhere else.
Spend ten unscripted minutes with the quality manager away from the sales team, and ask about a failure—any failure, ever, and what changed afterwards. Factories that inspect, record and correct talk about failures as process events. Factories that perform quality for audits talk about certificates. And cross-check one contract end to end: pick any running order, then follow its traveler to the test record to the packing list. Coherence there predicts coherence at your FAT.
Verification Methods Compared
Each vetting method catches a different class of problem, and the cost scale differs enough that the right mix depends on order size. The table is the version buyers work from.
| Method | What It Catches | Cost and Speed |
|---|---|---|
| Registry and certificate checks | Fake entities, expired or out-of-scope certificates, inflated histories | Near zero; days of desk work |
| Video factory tour | Staged or borrowed facilities; obvious capability gaps | Free; an hour, but staged footage deceives |
| On-site audit | Real capability, process discipline, and the coherence between claims and shop floor | A trip plus two days; the reference standard |
| Third-party inspection or audit | The same gaps when you cannot travel, with an independent report your bank accepts | Fixed fee; one to two weeks |
| Pilot order with witnessed testing | The full chainâproduction, documentation, packing, communicationâunder real stakes | Order value; the slowest but most honest test |
The methods stack. Desk checks plus a video tour qualify a factory for quotation; an audit or third-party report qualifies it for a first order; a pilot order with a witnessed FAT—our guide to why FAT matters for switchgear explains what to watch—qualifies it for the portfolio.
When a Factory Tour Is Not Enough
The audit has honest limits, and three of them matter. First, the borrowed line: some traders stage tours in a friendly factory that is not the one that will build your order. The counter is contractual—name the manufacturing site in the purchase order and make deviation a breach, then verify the nameplate and the traveler at FAT. Second, the peak-week effect: a factory can look disciplined during the week it expects you. Unannounced arrival times, a second visit on larger orders, and in-process records that predate your email asking for them are the practical antidotes. Third, the subcontracted step: even honest factories buy out operations they lack—tanks, cores, castings. That is normal and acceptable if disclosed; it is disqualifying if discovered.
The structural answer to all three is the same: shift trust from promises to verifiable events. Witnesses at testing, milestone payments against documents, site names in contracts—the vetting does not end at the audit; the audit simply tells you what to verify later.
The Pre-Order Action List
- Run the registry, certificate-source and export-data checks before shortlisting;
- Hold a technical conversation that requires factory knowledge, not a price conversation;
- Audit on site, or commission a third-party audit, before the first order above routine size;
- Name the manufacturing site and forbid undisclosed subcontracting in the purchase order;
- Structure payments against verifiable milestones—advance, after FAT, against documents, against arrival;
- Place a pilot order with witnessed testing before committing a portfolio to a new factory;
- Keep one contract end-to-end check—traveler to test record to packing list—as your recurring audit habit.
Conclusion
Vetting a Chinese equipment manufacturer is not a ritual of suspicion; it is how professional buyers match the confidence in their purchase order to the evidence behind it. Six dimensions, a handful of desk checks, one honest day in the workshop—the whole exercise costs less than a single week of project delay.
The factories worth buying from will make the process easy, because they have nothing to hide and everything to gain: every audit they pass is a competitor filtered out. Make the evidence standard part of your purchasing language, and the supply base you end up with will have selected itself for exactly the qualities no brochure can fake.
Frequently Asked Questions
The questions buyers ask most before qualifying a new Chinese equipment supplier.
Recent Posts
Power Cable Warranty Terms: What to Demand and What to Watch For
Power Cable Warranty Terms: What to Demand and What to Watch For Quick Answer: A usable warranty names its scope, duration, evidence standard, exclusions and
The Cable Sample Approval Process: What to Test Before Mass Production
The Cable Sample Approval Process: What to Test Before Mass Production Quick Answer: Sample approval tests the supplier’s claims while changes are still cheap —
Cable Drum Packaging for Export: Specs, Marking and Transit Protection
Cable Drum Packaging for Export: Specs, Marking and Transit Protection Quick Answer: Export packaging is a technical specification: drum size for weight and bend radius,