
Factory Witness Tests and Hold Points: What to Hold Before Release
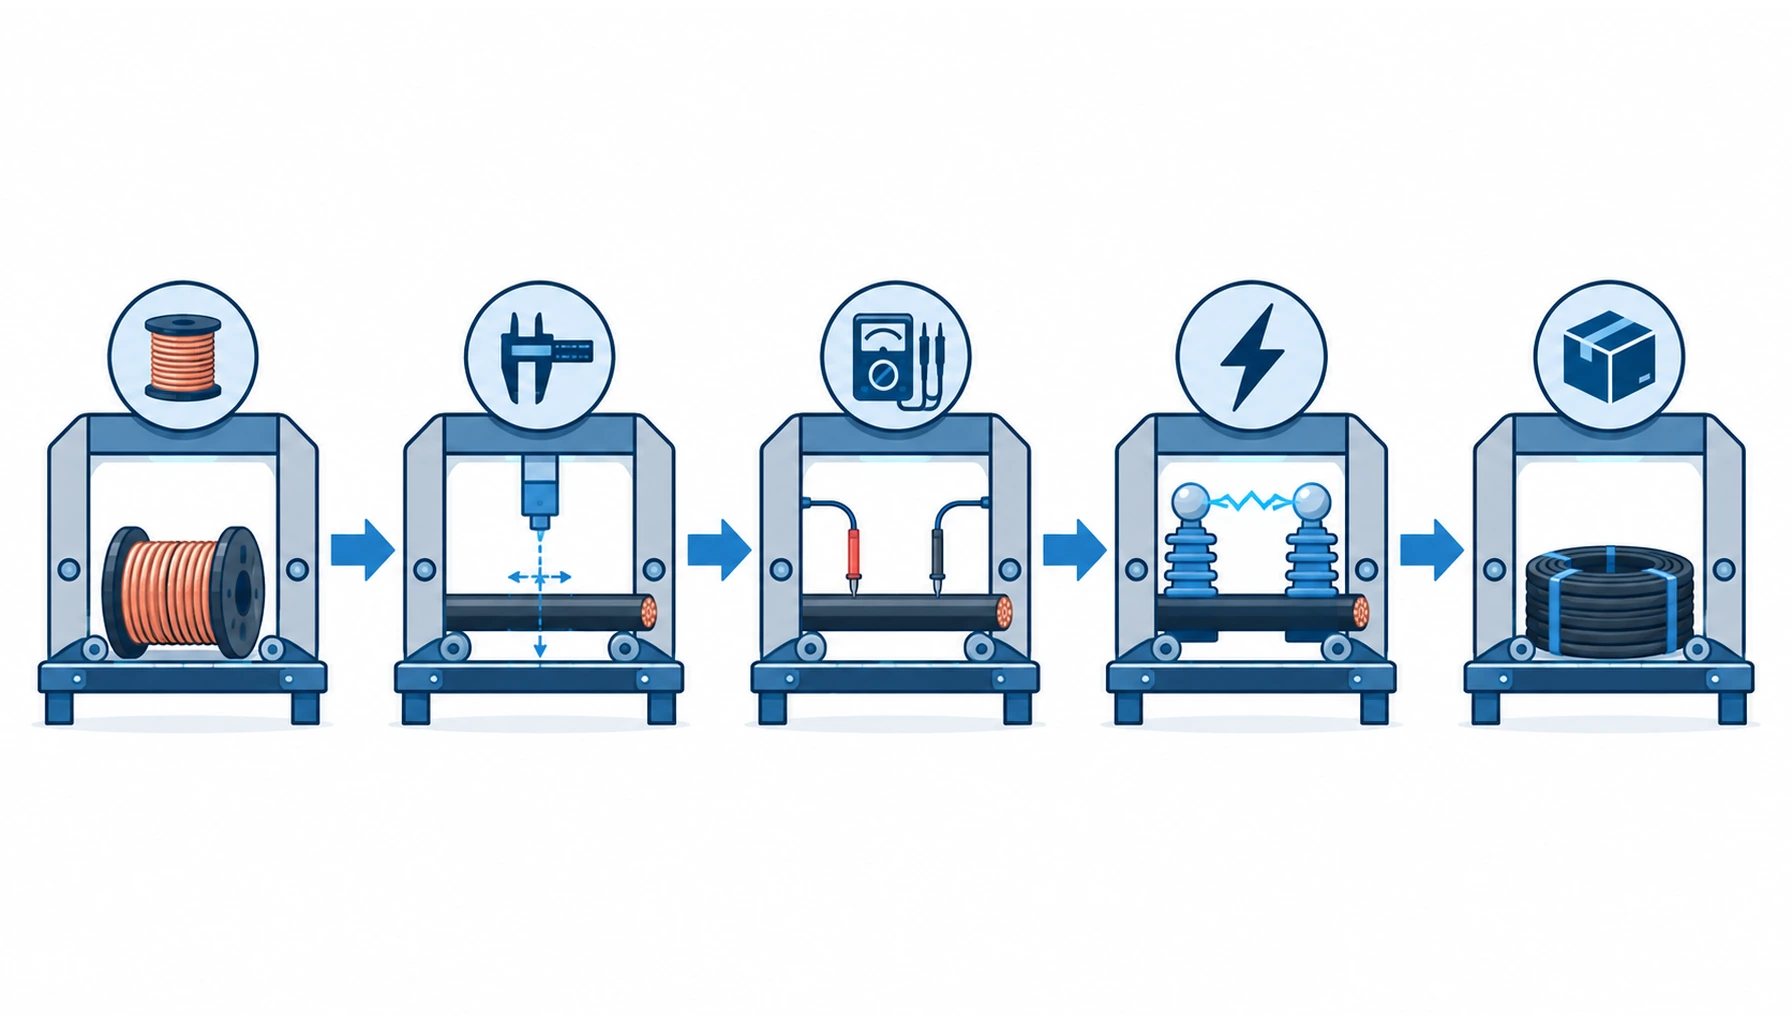
Quick Answer: A factory witness test is an inspection at the point where the cable is still at the factory and the buyer still has leverage. It earns its cost only when the hold points are named before the order is placed, sequenced so that each one blocks the next, and tied to an explicit release for dispatch.
Introduction
Most buyers accept test certificates and never see the test. That is usually the right call. It stops being the right call on a large or unusual order, where the cost of discovering a problem after dispatch is measured in weeks of programme rather than in the price of a drum.
This page is for procurement and quality staff who have to decide how far to go. It sets out what the factory tests as a matter of course, how to pick hold points that are actually useful, what to do on the visit, the documents that should travel with the goods, and the six decisions to freeze before the order is placed. The acceptance side of the same subject is covered in our note on factory and site acceptance testing, and the routine test arrangements are described in our note on cable factory testing.
What the Factory Tests Anyway
Routine tests run on the finished length. Conductor resistance, insulation resistance, continuity where required, and a high-voltage withstand test are performed on the completed drum as normal production practice. The results belong to the drum you are buying, and the test sheet is the record of them.
Type tests run once on a construction, not on your order. Fire performance, smoke density, halogen acid evolution, mechanical endurance and ageing behaviour are demonstrated on a representative sample, and the resulting report covers that construction rather than the drums on your order. It is evidence that the design is capable, not that the goods are good.
Some checks happen during manufacture rather than at the end. Conductor diameter, strand count, insulation thickness, concentricity and lay length are verified in process, because a dimensional defect found after the sheath is applied can only be seen by cutting the cable open. Those checks are cheap when they are routine and impossible when they are not.
What is not tested by default is anything the standard does not ask for. Special tests, extended samples, or checks on a specific parameter written into your specification sit outside the routine regime. If you need one, it has to be in the order, and the factory has to plan the sample. Our notes on the mechanical test methods and on halogen acid and smoke testing set out what those methods actually prove.
Witness Points: Where to Hold and Why
A hold point is a gate, not a meeting. It is a stage that cannot be passed until the buyer or their representative has seen the evidence and signed. A hold point that does not block anything is an appointment, and appointments get rescheduled.
Two or three well-chosen points beat a full itinerary. The useful ones are those after which the item cannot be corrected, or after which a failure is expensive to find. Routine electrical testing on the finished length is the classic example, because it is the last moment the drum is cheap to hold and cheap to rework.
Name who attends and who may sign. If the buyer’s own engineer attends, the release is immediate. If a third-party inspector attends, the report has to be issued and accepted before dispatch, which adds a day or two to the schedule. That time belongs in the plan rather than in an argument on the dispatch date. The different roles are compared in our note on third-party cable inspection.
Hold Points Compared
The table sets out the hold points available on an industrial cable order: what each catches, what to specify, the evidence to demand, what drives cost and time, and how each gives false assurance.
| Hold point | What it catches | What to Specify | Evidence to Demand | Cost and Lead-Time Driver | How It Misleads |
|---|---|---|---|---|---|
| Conductor and material verification | Wrong strand class, wrong metal or a conductor that does not match the declared schedule | The class, the conductor schedule and whether tinned strand is required | A measured strand count and diameter, with the copper purity statement | An hour of work and a sample cut from the run | A certificate of conformity read as proof instead of a measurement |
| In-process dimensional check | Thin insulation, eccentricity and lay lengths that will fail a mechanical duty later | The dimensions to be checked, the tolerance and the frequency | An in-process record with the readings and the time they were taken | Requires the check to be planned into the run, not added afterwards | One measurement at the start of a long run treated as covering all of it |
| Routine electrical tests | Low insulation resistance, open cores, a conductor resistance outside the standard | The test voltages, the durations and the acceptance figures | A signed test sheet per drum, with each core and the armour recorded | Bay time and the cost of holding the drum until results are read | A pass result read as proof the cable will survive installation |
| High-voltage withstand test | Weak points in the insulation that a low-voltage check will not stress | The voltage, the duration and whether it is applied to the finished length | The test record with the voltage trace and the duration noted | Slower than a routine check, and requires the drum to be held on the bay | Repeated testing at high stress, which can damage what it is meant to prove |
| Final inspection and packing | Wrong marking, damaged sheath, missing drum labels and packing that will not survive transit | The marking to appear on sheath and drum, and the packing standard | Photographs of drum ends, labels and packing, with the drum list | Hours rather than days, but it must happen before the container is loaded | A check done after loading, when correcting anything means unloading again |
Running the Witness Visit
Send the acceptance criteria in advance. A witness who arrives without the specification, the test plan and the acceptance figures is there to watch rather than to inspect. Give the factory the same documents, so the test can be run against a known requirement rather than a remembered one.
Watch the measurement, not the certificate. The value of attendance is seeing the reading taken on your drum. Ask for the instrument, the calibration status and the connection to the cable, then look at the figure and write it down yourself. A photograph of the meter display beside the drum label is worth carrying back.
Record what you saw, not just whether it passed. The readings, the ambient conditions, the drum numbers and the time. Insulation resistance in particular varies with temperature and moisture, so a figure without the conditions cannot be compared with anything later. Our note on insulation resistance testing explains the corrections.
Sign the release where the sequence allows it. Where a witness point is passed, the release should be given at the plant rather than by email three days later. On a phased order, the release applies to the drums presented, not to the whole contract.
Documents That Travel With the Goods
The test sheet is the minimum. One sheet per drum or per batch, whichever the order states, with the readings, the standard applied and the date. It should identify the drum numbers it covers so the evidence can be matched to the physical goods at site.
Declaration of conformity and material certification follow. A declaration states which standard the goods were made to and who is making the statement. Material certification supports the compounds and the conductor where the specification requires traceability. Both are office documents, and both are routinely promised and then chased. Naming them in the order and tying payment to them is what makes them arrive.
Marking and length records close the loop. The sheath marking, the drum label and the delivered length all have to agree with the order. Where length tolerance is written as a percentage of the total, our note on cable length tolerance explains how the measurement is usually stated, and our note on cable labelling and documentation covers what belongs on the label. Where the cable will be tested on site, the acceptance regime is described in our note on acceptance testing.
What to Freeze Before the Order Goes Out
Six decisions turn an inspection intention into a procedure that can be enforced. Each belongs in the purchase order.
| Decision | What to State | Evidence to Attach | Cost of Leaving It Open |
|---|---|---|---|
| Hold points and sequence | Which stages block progress, and the order in which they are released | A test plan showing each point and what it releases | An inspection that happens after the cable is already packed |
| Acceptance criteria | The figures that constitute a pass, per test and per parameter | The standard clause or the buyer's specification extract | A dispute about whether an out-of-tolerance reading actually failed |
| Attendance and authority | Who attends, who signs and how long after the test a release is issued | A named attendance list with signatory authority | A drum held on the bay waiting for a signature that has no owner |
| Third-party arrangements | Whether an independent inspector is required, and who engages and pays them | The inspection scope and the engagement terms | A report arriving after dispatch, with no leverage left |
| Documentation pack | Every document to be supplied with the goods, and the language | A document list with the issuing party for each item | A handover file assembled by email over several weeks |
| Non-conformance route | What happens when a drum fails, and who bears the rework and the delay | A written disposition procedure with timescales | A failed drum released on a promise, and a claim with no evidence |
Cost and Lead Time
Witnessing costs the factory money, and it is fair to price it. Holding a drum, preparing a test bay, running a test twice and having paperwork ready for a fixed date all consume capacity. A supplier who offers it free is either absorbing it into the unit price or not planning for it.
The buyer’s cost is in schedule, not in fees. Travel, a day of engineering time and a day or two of release time are small against the value of finding a problem before dispatch. Set against a container that has to be opened, unloaded, sorted and re-shipped, the arithmetic is almost always in favour of attending on the orders that matter.
Where the cost becomes real is repeated testing. A high-voltage test applied twice because the first result was not recorded, or a re-test because a witness arrived late, stresses the cable and delays dispatch for no additional evidence. Getting the sequence right the first time is the cheapest form of quality assurance on the order.
When Witness Testing Is Not the Answer
When the construction is standard and the supplier is approved. A routine product from a factory with a good record and complete test sheets does not need a visit. Put the effort on the orders that carry risk.
When the hold point is after the point of no return. Witnessing the final packing only confirms that a decision already made was executed. Move the attendance earlier, where a finding can still change something.
When nobody can attend. A hold point that nobody is available to release becomes a delay by default. Either appoint a competent representative, engage an inspector, or remove the hold point and rely on documents. The one option that does not work is keeping the gate and not staffing it.
When the test does not prove what is being bought. A test certificate for a slightly different construction, a sample taken from a different run, or a type report that predates a compound change all look like evidence and are not. On a comparable point in the equipment world, our note on why factory testing matters sets out how the same mistake is made, and the supplier capability question behind it is covered in our note on cable factory audit.
RFQ Checklist
- The hold points listed by name, with the stage each one releases
- The acceptance criteria for every test, stated as figures not descriptions
- Which tests are routine, which are type tests, and where the reports come from
- The conductor schedule and the measured verification required against it
- The in-process dimensional checks, their frequency and their tolerances
- The test voltages and durations, and whether testing is on the finished length
- Who attends, who signs, and the authority each signatory holds
- The notice required to book a witness slot, and the factory calendar date
- Whether an independent inspector is required, and who engages them
- The document pack, with the issuing party and the language for each item
- Sheath marking, drum labelling and the drum list with measured lengths
- The disposition route for a failed drum, with timescales and cost responsibility
Conclusion
A factory witness test is not a substitute for a good supplier, and it is not a formality either. It is a small, well-defined purchase of certainty at the only point in the chain where a finding is still cheap to act on. Named hold points, published criteria and a release that means something are what turn a visit into an inspection.
Kexingyu Cable Group (KXYE) has manufactured cable in Quanzhou since 1996 and runs routine and type testing in house, with hold points scheduled to buyer requirements and test records issued per drum. Send us the test plan and the criteria you work to, and we will confirm which points we hold, when, and what the record will contain. A request for quotation is the fastest route.


