
Auditing an Industrial Cable Supplier: Capability, Not Paperwork
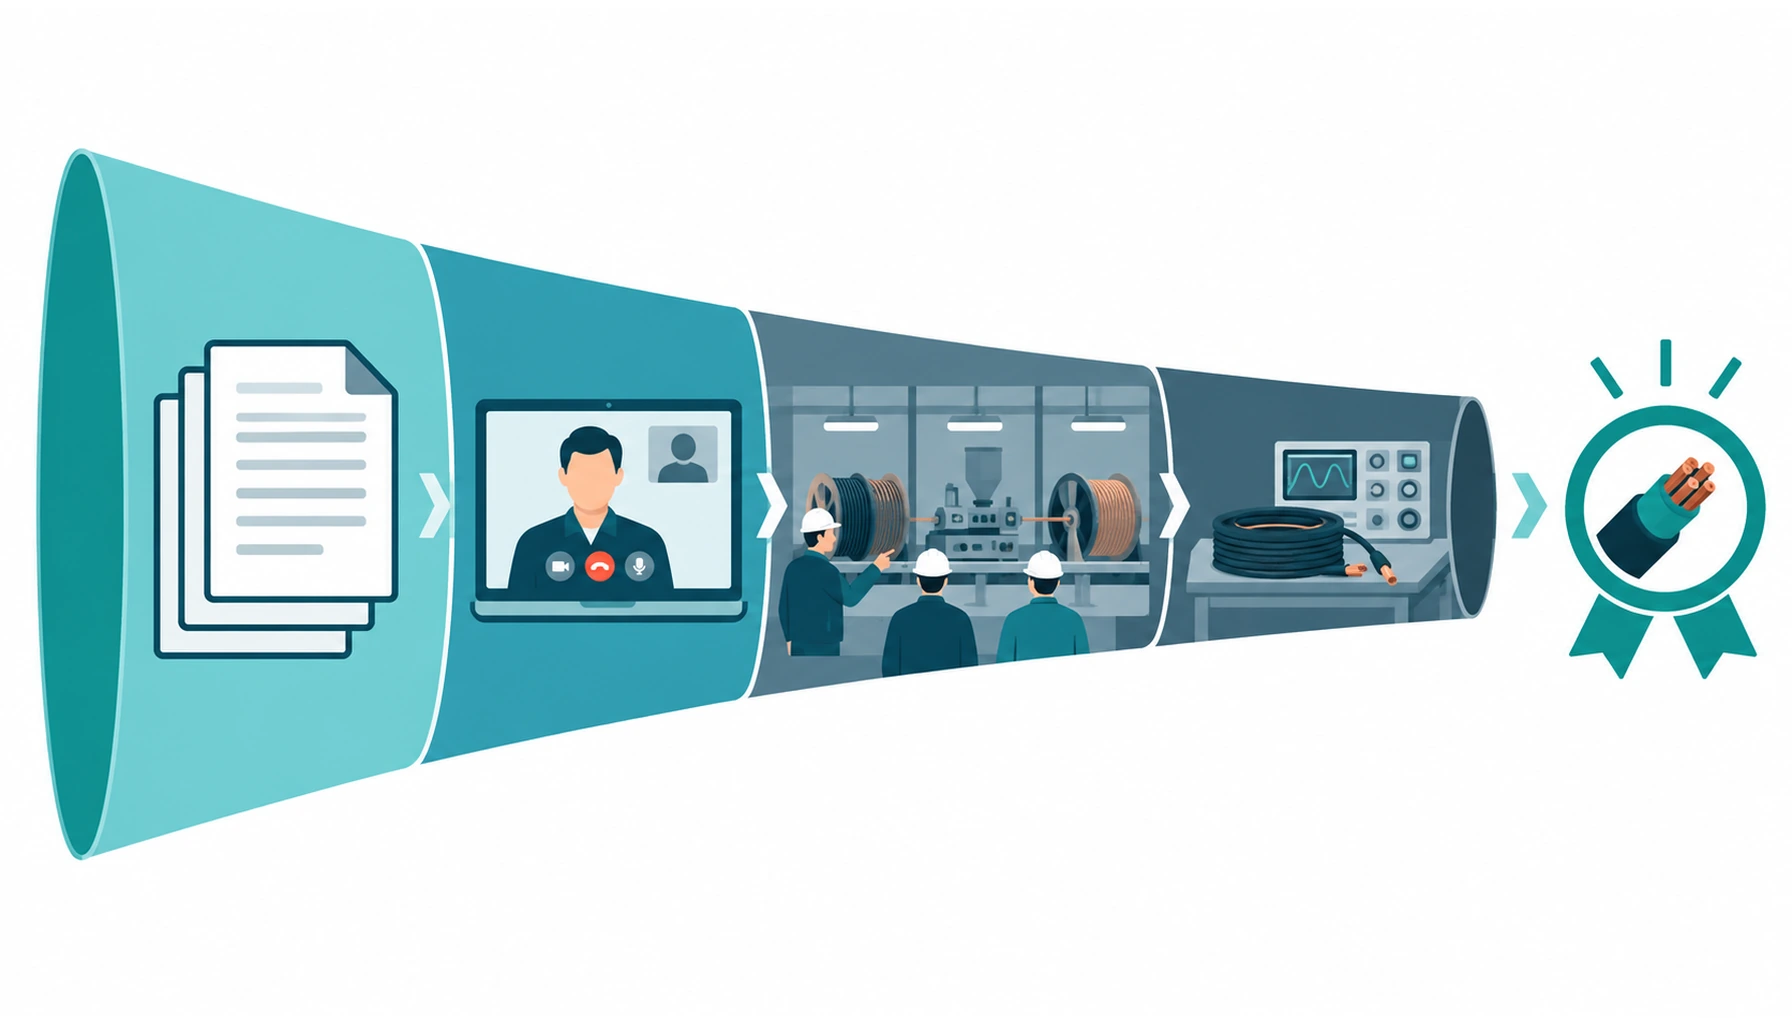
Quick Answer: A cable supplier audit is meant to answer one question: can this factory actually make and test the cable on the order, on the date promised, more than once. Certificates are the easy part. Capability lives on the production floor, in the calibration records, in the compound store and in the drawing revision list, and that is where the useful half hour of an audit is spent.
Introduction
Most EPC and site buyers audit a cable supplier once, under time pressure, with a checklist that rewards documents over capability. The supplier arrives at the next project with a folder of certificates, and nothing has actually changed about whether they can run the order through their line and hold the schedule.
This page is for buyers and project engineers running a supplier qualification or a pre-award audit. It covers what an audit is actually for, the difference between paperwork and capability, what to look at on the production floor, the audit routes and what each one proves, testing and traceability, the continuity questions that decide whether the second order goes as well as the first, and the six decisions to freeze before the order is placed. The commercial background is covered in our note on checking a cable manufacturer.
What an Audit Is Actually For
An audit reduces a specific risk, and the risk should be named first. On a first order from an unknown factory, the risk is capability, so the audit looks at plant, personnel, calibration and test facilities. On a repeat order from a known factory, the risk is continuity, so the audit looks at capacity, staffing and the order book instead.
It is not a certification exercise. A valid certificate proves that at some point a management system or a product type met a standard. It does not prove that the line making your drum is running to the approved drawing this week. The certificate is a starting point, not the finding.
The output is a decision, not a score. An audit that produces a percentage and no view on whether the supplier can deliver is wasted. The useful output is a short list of risks with owners, and a decision on whether to award, award with conditions, or look elsewhere.
Paperwork Versus Capability
Documents to read before the visit. The quality manual matters less than the drawing register, the revision control process, the calibration schedule and the last two internal audit reports. Those four show whether the system is alive or ceremonial, and they are quicker to read than a manual.
The questions a folder cannot answer. Who signs a change to a construction, and how does the change reach the shop floor? What happens to a drum that fails a routine test? Where is non-conforming compound or part-finished cable kept? How long does a compound batch sit before use? These are answered by walking the floor, not by reading a certificate.
Test capability is the sharpest test of all. A factory that owns its test bay, maintains its instruments and can show calibration records to a traceable standard is a factory that knows what it is shipping. Where every test is subcontracted, the release paperwork becomes a forwarding exercise and the technical answers get thinner, which is the pattern described in our note on manufacturers compared with trading companies.
What to Look At on the Production Floor
The conductor side first. Wire drawing and stranding, the number and diameter of wires against the specified class, and how the factory checks them. A stranding line that cannot show a measured sample against the drawing is a warning sign, because every other property of the cable depends on that conductor.
Then the extrusion and the drumming. Insulation and sheath lines running at a controlled speed with an inline diameter measurement, and a drumming station that measures length by counter or by weight against a calibrated scale. Length control is one of the most common sources of disputes at receipt, and the method used is described in our note on cable length tolerance.
Finally the test bay and the quarantine area. An operating high-voltage test set, a resistance bridge, and instruments with calibration labels in date. Beside it, a clearly separated area for material or drums that failed something. A factory with no visible quarantine area has one, it is just not labelled, and that is the kind of thing an audit exists to find. What normally happens at these stations before release is set out in our note on factory testing.
Audit Routes Compared
The table compares the routes available for qualifying an industrial cable supplier, what each one actually proves, what to specify, the evidence to demand, what drives cost and time, and how each one fails.
| Route | What it proves | What to Specify | Evidence to Demand | Cost and Lead-Time Driver | How It Fails |
|---|---|---|---|---|---|
| Document review at desk | That a system, certificate and drawing register exist on paper | The document list, the revision register and the calibration schedule | Current certificates and the last two internal audit reports | Nearly free and quick, but the weakest single route | A tidy folder attached to a floor that does not follow it |
| Remote walkthrough | That the plant exists and the main lines are in place | The areas to be shown, live, and the questions to be answered | A recorded session plus photographs of the named stations | Low cost, no travel, but easy to stage and edit | A rehearsed route that skips the quarantine and calibration areas |
| On-site capability audit | That the plant, people and test facilities can run the order | The audit scope, the criteria and the people to interview | A signed report with findings, risk ratings and owners | Travel and staff time, with a few days of programme | A walk-through with no measurement, which finds nothing |
| Trial order with witnessed test | That the factory can make and test this specific construction | The construction, quantity, test protocol and the witness point | A production sample, the test report and the retained sample | A production slot and a witness visit, the real cost of the route | A trial made carefully by hand, not on the production line |
| Performance review over time | That the supplier holds quality and schedule on repeat orders | The metrics, the reporting period and the review meeting | On-time delivery, rejects and claim history by quarter | Administration only, but it needs two or three orders to work | Metrics collected but never acted on, so nothing improves |
Testing, Traceability and Records
Ask what the release package contains, then ask to see one. A routine test certificate, a resistance measurement, a dimensional check and a drum schedule are the minimum. Seeing an actual package from a real order, with the drum numbers matching, tells you more than a description of the process.
Calibration is where weak factories show. Ask for the calibration certificates for the diameter gauge, the length counter, the resistance bridge and the high-voltage set, and check the dates. Instruments out of calibration do not make a test invalid on its own, but they show how the factory treats measurement, which is the substance of the audit.
Traceability has to survive the journey. The drum number on the label should lead to the production record, the compound batch, the test result and the release note. Where a factory cannot demonstrate that chain from a finished drum, expect the same gap to appear at site if a claim is ever raised, which is the point our note on cable factory audit practice returns to.
Commercial and Continuity Questions
Capacity and the order book. How many extrusion lines run, on what shift pattern, and what is already committed for the next quarter. A factory that is comfortable today can become a bottleneck when two large orders land in the same month, and the audit is the moment to ask.
Single points of failure. One compound supplier, one test set, one person who knows the drawing register, one stranding line for a long lay length. Any of these can stop an order, and the answer to give a project manager is whether a second source exists and how quickly it can be brought in.
Subcontracting and changes. Ask directly what is outsourced, because a factory that subcontracts part of the process is responsible for the result even where the work is done elsewhere. Ask also how a change to a construction is notified, since an unannounced substitution of a compound or a filler is the change that most often reaches site without anyone noticing.
What to Freeze Before the Order Goes Out
Six decisions turn an audit into something the order can rely on. Each belongs in the enquiry or the purchase order.
| Decision | What to State | Evidence to Attach | Cost of Leaving It Open |
|---|---|---|---|
| Audit scope and timing | Which route is used, when it happens and what it covers | An audit plan with the criteria and the named stations | A qualification that proves nothing about the line making your drum |
| Release package | The exact test and document set issued with every drum | A specimen release package from an earlier order | A delivery with certificates that cannot be traced to the drums |
| Traceability chain | What links drum number to compound batch and test result | A worked example from the factory records | A claim that fails because the evidence cannot be tied to the goods |
| Change control | How a construction change is notified and approved | The written notification process and the approval point | An unannounced compound or filler substitution found after delivery |
| Capacity commitment | The slot reserved for the order and the dispatch plan | A dated production schedule signed by the factory | A promised date that slips when other orders arrive first |
| Second source position | Whether a qualified alternative exists and when it is revisited | A qualification file for at least one alternative supplier | A single point of failure that stops the programme at the worst moment |
Cost and Lead Time
An audit costs less than one failed delivery. A day of plant time and travel is a small number against a rejected drum, a re-order and a delayed pull. The return is not the audit fee, it is the defective order that never happens.
Audit late and you pay twice. An audit run after the order is placed cannot change the supplier, only the argument. The value of the exercise comes from doing it before award, when there is still somewhere else to go.
The trial order is the route that earns its cost. A small production order with witnessed testing costs a production slot and a visit, and it tells you more about a factory than any document. For a first order of real value, it is usually the cheapest risk reduction available. How it fits with sample approval is covered in our note on the sample approval process.
When a Full Audit Is Not the Answer
When the order is small and repeat. A short tail order from a supplier you already use does not need a fresh audit. Track performance instead, and spend the audit budget where the risk is.
When the audit would replace a specification. A good audit does not fix a poor specification. If the construction, class and test standard are not written down, a capable factory will still make the wrong cable, and the argument will be about interpretation rather than ability.
When the certification is already the requirement. On regulated work, the certificate that matters is the product certification for the market, not the factory’s quality system. Those are separate questions, and the market-specific set is described in our note on product certifications for cable.
When the real issue is price. Chasing a price that the factory cannot sustain ends in substitutions, thin margins on freight or a schedule that gives way. An audit should confirm that the quoted price can actually be built at, which is a different exercise from finding the cheapest source, and one that our note on common sourcing mistakes deals with directly.
RFQ Checklist
- The audit route, its scope and when it will be carried out
- The production lines and test stations the audit must cover
- The calibration records to be produced, and the standard they trace to
- The release package issued with every drum, with a specimen copy
- The traceability link from drum number to compound batch and test result
- The notification process for any change to the approved construction
- The trial order quantity, if one is required, and its witness point
- The production slot reserved and the dispatch plan for the order
- The capacity available in the delivery month, not only at enquiry
- What is subcontracted, and how that is controlled and declared
- The identity of the technical contact who answers an audit finding
- Whether a qualified second source exists, and when it is reviewed
Conclusion
A cable supplier audit is worth the day it takes when it is aimed at capability and timed before award. The certificate tells you a system exists. The floor, the calibration labels, the quarantine area and a worked traceability example tell you whether the cable on your order will come out right, and whether the next order will go the same way.
Kexingyu Cable Group (KXYE) has manufactured cable in Quanzhou since 1996 and runs drawing, stranding, extrusion, drumming and testing on its own lines, so an audit is answered from the production record rather than from a folder. Our background is set out on the company page, and a request for quotation is the fastest route to start one.


